


 English
 русский
 Español
 عربى

Steel is the backbone of modern manufacturing, yet it is never a single, uniform material. When engineers and buyers ask, "How can you clas...
READ MORE
News
Home / Author / Chen Ruoxi — Overseas Product Sales Manager / Precision Circular Stamped Parts with a Central Hole for Reliable Industrial Assembly
Precision Circular Stamped Parts with a Central Hole for Reliable Industrial Assembly
2026-08-31
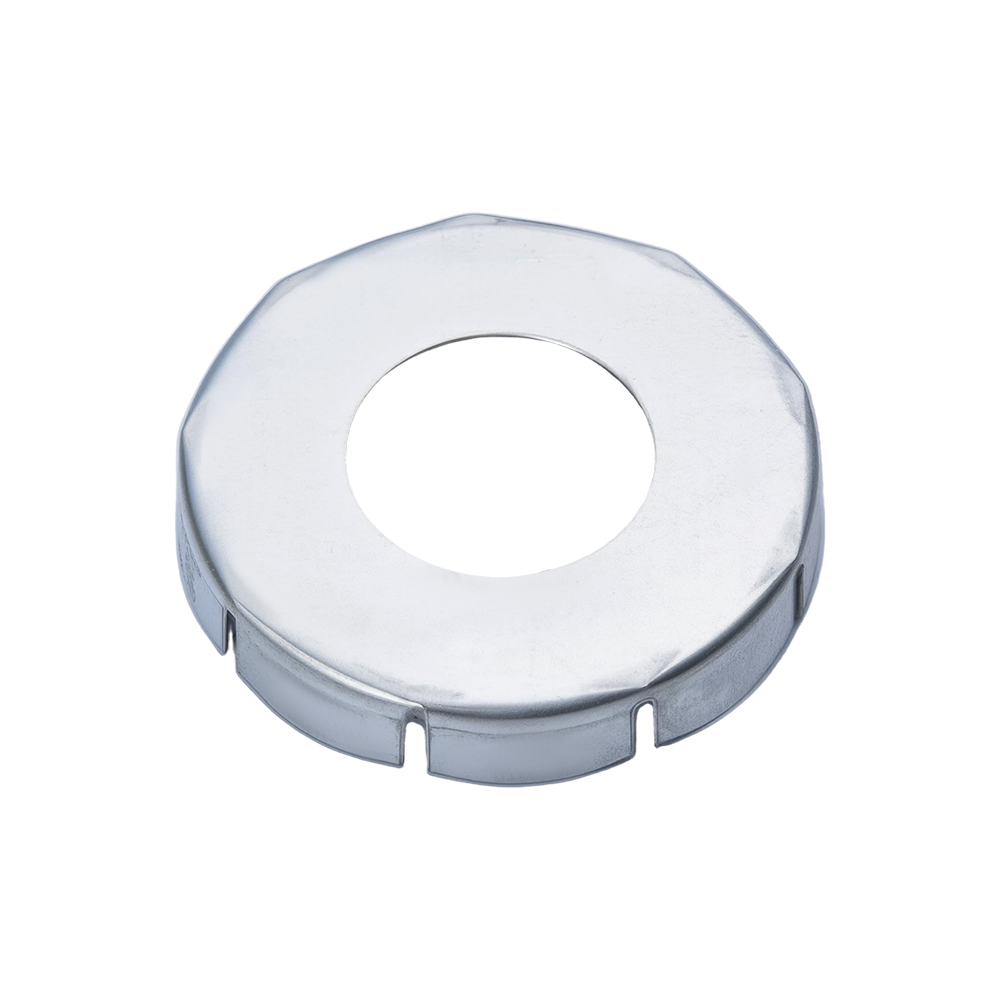
Circular stamped parts with a central hole are compact but highly functional metal components used in assemblies that require accurate positioning, dependable fastening, and repeatable mechanical performance. Their simple circular geometry allows them to support, connect, reinforce, separate, guide, or secure other components. When produced with controlled stamping processes, these parts can deliver consistent dimensions in high-volume applications while maintaining an economical production cost.
Yuyao Hongli Optoelectronics Co., Ltd. manufactures customized circular stamped parts for customers in automotive, electrical, machinery, construction, household appliance, optical instrument, and general hardware industries. The company combines more than 20 years of manufacturing experience with modern stamping workshops, engineering support, quality control, and flexible OEM/ODM production. Its capabilities cover stamped parts, deep-drawn parts, bending parts, kitchen appliance accessories, and automotive stamping parts.
The central hole is one of the most important functional features of this product. It may be used for a screw, rivet, bolt, shaft, pin, threaded connection, locating feature, or other fastening method. Depending on the application, the hole may be produced as a simple through-hole or incorporated into a more complex stamped geometry. The outside diameter, thickness, hole diameter, edge profile, surface condition, and overall shape can be developed according to customer drawings, samples, or technical requirements.
Although these components appear straightforward, their performance depends on careful control of material selection, tooling design, press settings, piercing quality, dimensional accuracy, burr management, and inspection. A poorly produced circular part may create misalignment, looseness, excessive friction, assembly delays, or premature failure. A properly engineered part, by contrast, can improve the reliability of the complete product while reducing assembly cost and simplifying inventory management.
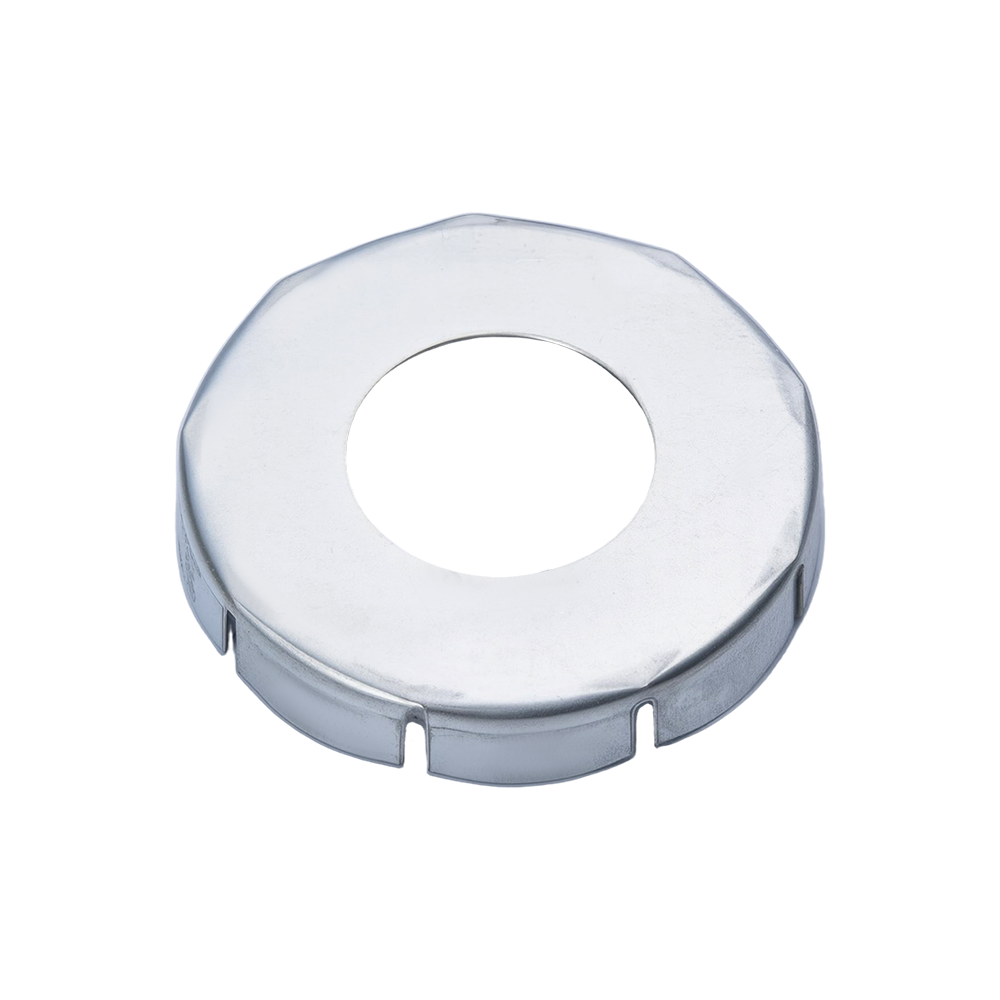
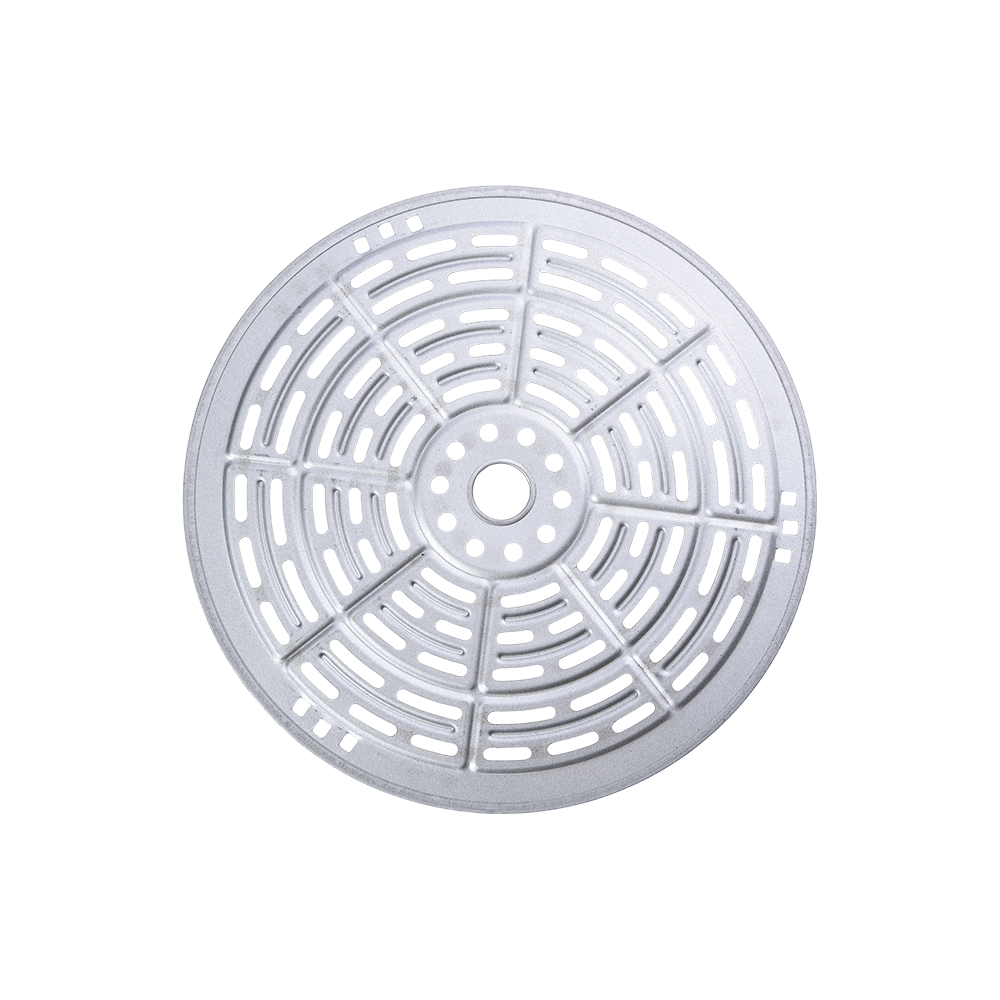
Circular stamped parts with a central hole
Product Overview and Functional Design
A circular stamped part with a central hole is generally formed from sheet metal or strip metal through one or more operations in a stamping die. The basic part consists of an external circular profile and a concentric or specified central opening. Additional features may be added when required, including shallow steps, raised sections, countersinks, embossed areas, notches, tabs, bends, or other formed details.
The component can serve many different purposes. In a fastening application, it may act as a washer-like support that distributes pressure over a larger area. In a mechanical assembly, it may function as a spacer, retaining element, guide, bearing support, mounting plate, or alignment component. In electrical equipment, it may provide a structural mounting point or help connect internal parts. In household appliances, it may support knobs, shafts, heating-related assemblies, covers, brackets, or other operating mechanisms.
The central hole can be located precisely in relation to the outside diameter. This relationship is particularly important when the part is used for rotation, alignment, or concentric assembly. Hole position accuracy helps reduce assembly stress and prevents components from being mounted off-center. For parts installed on a shaft or secured by a bolt, an accurately sized hole also reduces unwanted movement while allowing the assembly to be installed efficiently.
Customers may specify the product through a two-dimensional drawing, three-dimensional model, physical sample, written specification, or application description. Important parameters commonly include material grade, material thickness, outside diameter, hole diameter, flatness, concentricity, edge condition, surface finish, hardness, corrosion resistance, packaging, and annual quantity. When the customer does not have a complete drawing, the manufacturer can support the development process by reviewing the intended function and proposing a practical stamping solution.
Common Geometric Options
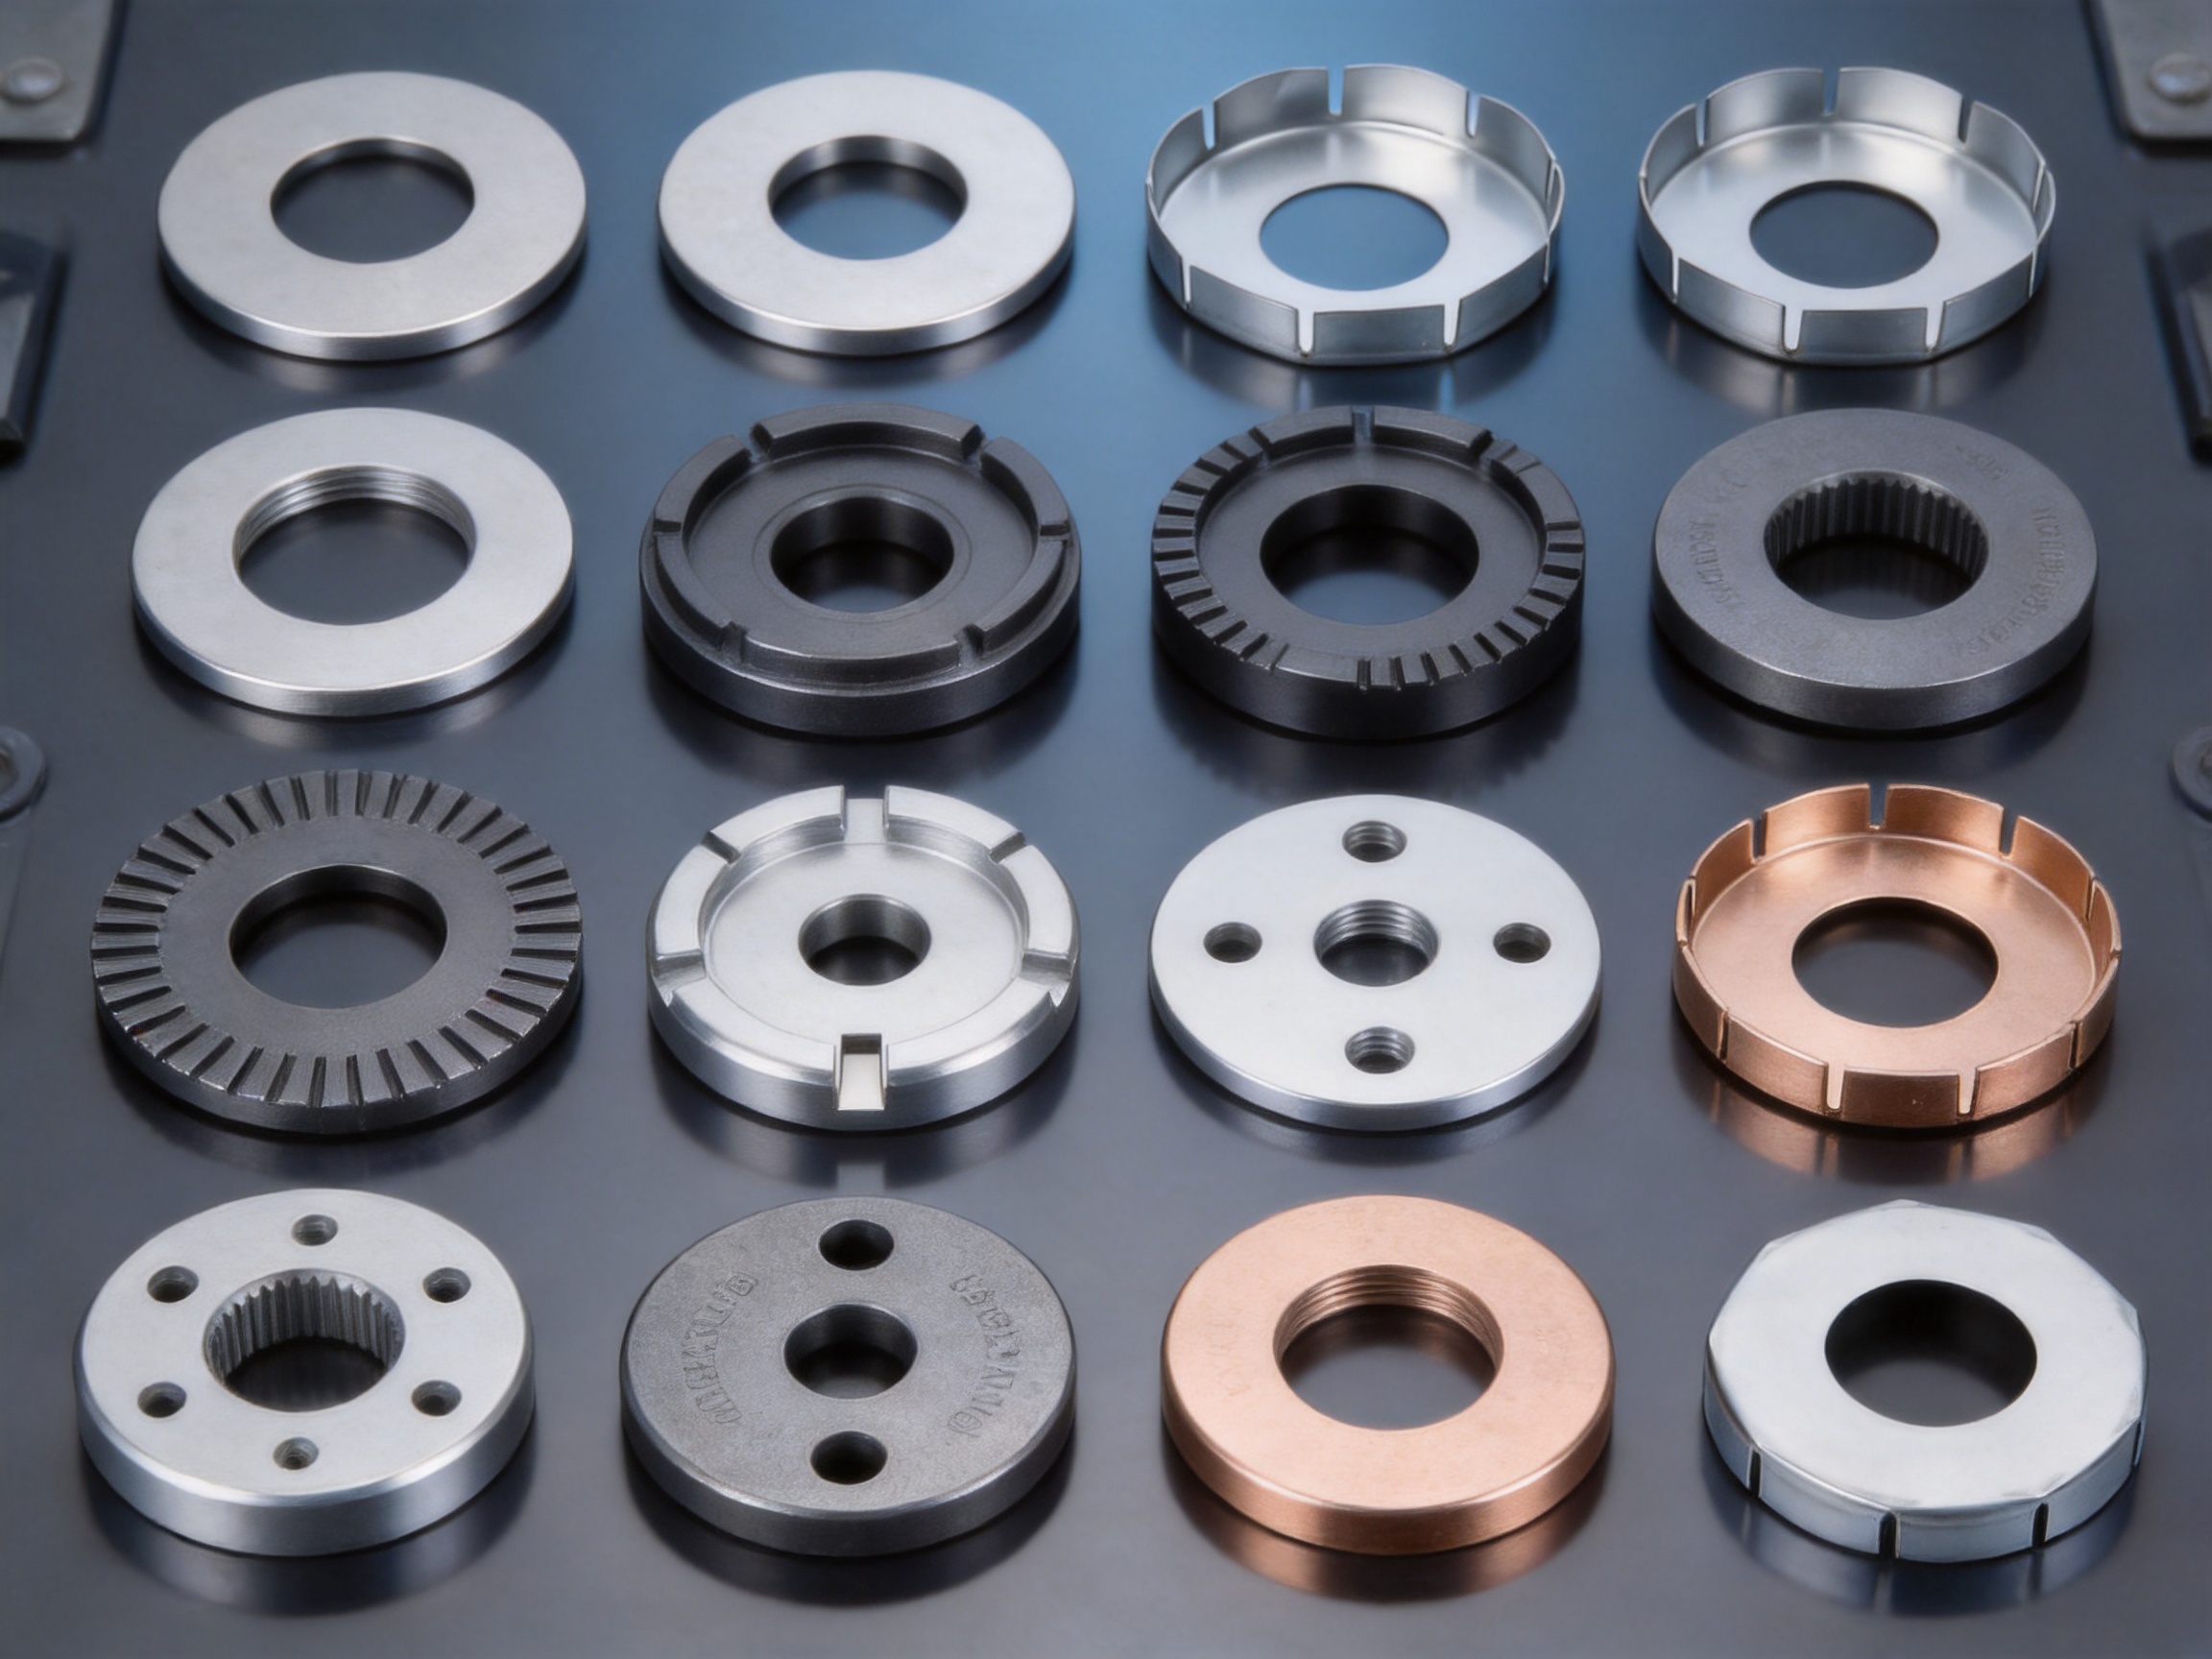
The simplest version is a flat circular disc with a central hole. This design is suitable for applications requiring basic fastening, spacing, or load distribution. A second option includes a formed shoulder or step around the hole. This feature can improve positioning or create a controlled distance between mating surfaces. A third option may include a countersunk or chamfered hole for flush-head fasteners. Other designs can incorporate small tabs, indexing notches, raised rings, or peripheral bends.
The best geometry depends on the role of the component. A part that only distributes clamping force may require a flat profile and smooth edges. A part used as a locating element may need a tighter relationship between the hole and outer diameter. A part exposed to repeated movement may benefit from a smooth surface, controlled hardness, and carefully managed burrs. A part installed in a thin sheet assembly may need additional forming features to prevent rotation or improve retention.
Stamping tooling is developed around the required geometry, material behavior, production quantity, and dimensional tolerance. The design may use a single-operation die for a simple part or a progressive, compound, or multi-stage process for more complex features. Selecting the appropriate tooling structure helps balance tooling cost, cycle time, quality, and long-term production stability.
Advantages of Circular Stamped Parts with a Central Hole
Efficient High-Volume Production
Stamping is well suited to repeated production because the forming operation can be performed quickly and consistently once the tooling has been established. Compared with individually machining every circular component, stamping can reduce processing time and material handling for suitable geometries. This makes it especially advantageous for appliance, automotive, electrical, and hardware programs that require stable quantities over an extended period.
High-volume efficiency is not limited to machine speed. A well-designed stamping process also reduces the number of separate operations required to manufacture each part. Cutting, piercing, forming, and other features can be integrated into an organized production sequence. Fewer handling steps can help reduce variation, shorten lead times, and simplify production planning.
Consistent Dimensions and Repeatability
Industrial assemblies often require thousands or millions of similar components. Manual or loosely controlled production methods may lead to variations in hole diameter, circularity, thickness, or outer profile. Precision stamping uses dedicated tooling to repeat the same geometry across production batches. This repeatability supports automated assembly and reduces the need for manual sorting or corrective fitting.
Consistent parts also make it easier for customers to maintain stable assembly settings. Fastening equipment, insertion tools, shafts, and fixtures can be designed around a predictable component. When incoming parts remain within the agreed specification, production interruptions and rejection rates can be reduced.
Customized Central Hole Sizes
The central hole does not need to follow a one-size-fits-all standard. It can be customized to match a bolt, rivet, shaft, pin, tube, threaded insert, or other mating feature. The hole can also be coordinated with the material thickness and outside diameter to preserve sufficient strength around the opening.
Customization is particularly useful when an assembly has limited space or when a standard washer or commercially available disc does not provide the required fit. A purpose-made stamped component can combine the exact hole size with the correct outer diameter, profile, material, and surface treatment. This can eliminate modifications during assembly and create a more integrated product design.
Strong Functionality in a Compact Form
The circular format provides a favorable relationship between size, strength, and material use. A ring-shaped or disc-shaped component can distribute loads around a central connection while occupying limited space. The design is also compatible with many rotational and concentric assemblies.
When additional forming features are included, the part can perform several functions at once. For example, it may support a fastener, establish a fixed height, prevent movement, and guide a mating component. Combining these functions in one stamped part can reduce the number of components in an assembly and improve manufacturing efficiency for the finished product.
Material and Surface Flexibility
The material can be selected according to the application’s mechanical, environmental, electrical, and appearance requirements. Depending on the customer’s specification, suitable sheet materials may include carbon steel, stainless steel, galvanized steel, aluminum, copper alloys, or other metal grades compatible with stamping. The exact selection should be confirmed through engineering review because strength, ductility, corrosion resistance, conductivity, thickness, and formability all affect performance.
Surface treatment can also be considered where required. Options may include cleaning, deburring, polishing, plating, coating, passivation, or other finishing methods selected according to the operating environment. Surface requirements are especially important for parts exposed to moisture, temperature changes, chemicals, friction, or appearance-sensitive applications.
Cost Control Through Tool-Based Manufacturing
Once the die and process have been validated, the cost per piece can become highly competitive for medium- and large-volume production. Tooling distributes the forming force and guides the material accurately, allowing the same design to be reproduced efficiently. Compared with complex machining of each individual part, stamping may provide lower unit costs and shorter cycle times for suitable shapes.
Cost effectiveness also comes from designing the material layout carefully. Strip progression, nesting, blank size, and scrap management influence the amount of raw material used. Experienced process engineers can review the part design and identify ways to reduce waste without compromising strength or dimensional performance.
Manufacturing Process for Precision Circular Stamped Parts
1. Technical Review and Application Analysis
Production begins with an evaluation of the customer’s requirements. The manufacturer reviews the drawing, sample, digital model, or written description and identifies the part’s critical dimensions and functional surfaces. Particular attention is given to the central hole, outside profile, material thickness, flatness, concentricity, and any formed details.
The application is also considered. A component used in a static household appliance may have different requirements from one installed in an automotive mechanism subject to vibration and temperature variation. A part used near an electrical connection may require suitable conductivity or insulation-related surface control. Understanding the application helps ensure that the proposed manufacturing method is aligned with actual operating conditions.
2. Material Selection
Material selection affects every stage of production. The material must be strong enough for the intended load but sufficiently formable for the required stamping operations. Thickness influences stiffness, hole quality, edge condition, and the amount of force needed from the press. Surface condition can affect appearance, friction, corrosion behavior, and coating performance.
For customers with a specified material grade, production can follow the approved standard and incoming inspection requirements. For customers seeking a recommendation, the manufacturer can compare available options based on strength, corrosion resistance, conductivity, weight, formability, cost, and expected service conditions. Material certificates and inspection procedures may be incorporated into the quality plan when required by the project.
3. Tooling and Die Development
Tooling is central to the quality of a stamped circular component. The die must guide the sheet accurately, maintain the intended profile, and produce a clean central hole. Die clearance, punch geometry, cutting edge condition, guide structure, and material support all influence the finished part.
For a simple flat part, a compound die may be suitable because blanking and piercing can occur in a coordinated operation. For larger quantities, a progressive die may feed strip material through multiple stations, completing several operations in sequence. For parts with formed sections, additional stations may be used for drawing, bending, embossing, or calibrating the geometry.
Tooling design must also consider maintenance. Wear components should be accessible for inspection and replacement. A maintainable die helps protect long-term production stability and reduces the risk that gradual tool wear will create dimensional drift. Regular cleaning, lubrication where appropriate, sharpening, and preventive maintenance help preserve the intended part quality.
4. Sheet Preparation and Feeding
Before stamping, the material is prepared in coils, strips, blanks, or sheets according to the selected production method. Feeding equipment must deliver the material at a controlled position and pitch. Accurate feeding is important because even a small shift can affect hole location, outer diameter, or the relationship between multiple features.
Material handling should also protect the surface from unnecessary scratches, dents, and contamination. Clean and organized feeding improves the consistency of the process. When the production line is arranged for efficient flow, operators can monitor the operation more effectively and respond quickly to abnormalities.
5. Piercing and Blanking
The central hole is commonly produced by piercing, while the external circular profile is created by blanking. These operations can be performed separately or within the same die, depending on the part design and production plan. The cutting action must be controlled to produce a suitable sheared zone and manageable fracture zone.
Hole quality is influenced by material properties, die clearance, punch condition, press alignment, and lubrication. Excessive clearance can increase burrs and reduce dimensional accuracy. Insufficient clearance may increase cutting force, accelerate tool wear, or create undesirable deformation. Proper setup and inspection are therefore essential to maintain a clean and stable central opening.
6. Forming and Secondary Operations
If the component includes a raised ring, shoulder, countersink, bend, notch, or embossed feature, additional forming operations may be introduced. These operations are planned to prevent cracking, wrinkling, distortion, or loss of flatness. The order of operations is important because one forming step may influence the dimensions of another feature.
Some parts can be completed in a single integrated stamping sequence. Others may require secondary processes such as deburring, calibration, tapping, riveting, welding, cleaning, or surface treatment. The correct sequence depends on the product’s technical requirements and the desired balance between efficiency and quality.
7. Deburring and Edge Management
Stamping naturally creates a cut edge, and the condition of that edge must be suitable for the intended application. Burrs can interfere with assembly, damage mating surfaces, create safety concerns, or affect electrical clearance. The required edge condition should therefore be defined during the design stage.
Depending on the specification, deburring may be achieved through tooling optimization, tumbling, brushing, grinding, vibratory finishing, or another suitable method. Not every application requires the same degree of edge treatment. A carefully chosen process avoids unnecessary cost while ensuring that the component performs safely and reliably.
8. Surface Treatment and Protection
Surface treatment is selected according to corrosion exposure, appearance, friction, conductivity, and compatibility with the final assembly. Some parts may be used in their stamped condition, while others may require additional cleaning or coating. When a coating or plating is specified, dimensional effects must be considered, particularly around the central hole and other close-fitting features.
Proper handling after finishing is also important. Components should be protected from contamination, impact, and moisture during storage and transportation. Packaging may be customized to prevent tangling, scratching, deformation, or mixing of different part numbers.
9. Inspection and Process Control
Quality control should cover both incoming material and finished components. Typical inspections may include outside diameter, central hole diameter, thickness, flatness, concentricity, burr height, surface condition, formed height, and visual appearance. The inspection method and frequency can be adapted to the customer’s quality agreement and product risk.
Process control is more effective when quality is built into each stage rather than checked only at the end. Operators and inspectors can monitor the first-off sample, in-process samples, tool condition, material feed, and production records. If a trend is detected, corrective action can be taken before a large quantity of nonconforming parts is produced.
Yuyao Hongli Optoelectronics maintains a manufacturing structure that combines production experience, dedicated workshops, and quality management. Its factory covers approximately 5,000 square meters and employs more than 60 people. These resources support stable production, customer communication, and the conversion of approved designs into repeatable components.
| Manufacturing Stage | Primary Objective | Typical Quality Focus |
|---|---|---|
| Technical review | Confirm functional and dimensional requirements | Drawing interpretation, critical features, application conditions |
| Material preparation | Provide suitable sheet or strip stock | Material grade, thickness, surface condition, certificates |
| Tooling development | Create stable and repeatable forming operations | Die clearance, alignment, wear resistance, maintainability |
| Piercing and blanking | Produce the central hole and circular profile | Hole size, outer diameter, burrs, concentricity |
| Forming | Add shoulders, bends, embossments, or other features | Height, angle, flatness, cracking, distortion |
| Finishing | Meet edge and surface requirements | Deburring, cleanliness, coating, corrosion protection |
| Final inspection | Verify conformity before shipment | Dimensions, appearance, quantity, packaging, traceability |
Competitive Advantages Compared with Alternative Production Methods
Compared with General-Purpose Washers
Standard washers are convenient for common fastening applications, but they may not meet the exact requirements of a specialized assembly. Their outside diameter, inside diameter, thickness, material, and surface finish are limited to available standard sizes. A circular stamped part can be designed around the actual product rather than forcing the product design to accommodate a standard component.
Custom stamping can also add functional features that a conventional washer does not provide. A raised shoulder, anti-rotation notch, locating tab, special edge, or formed profile may allow one custom part to replace multiple standard pieces. This can reduce assembly steps and make the finished product more compact.
Compared with Machined Components
CNC machining can produce highly precise circular parts and is valuable for complex geometries, prototypes, and low-volume production. However, machining removes material and may require more time for each component. For suitable sheet-metal designs, stamping can offer higher production speed and lower unit cost once tooling has been completed.
Stamping is especially attractive when the part is thin, relatively flat, and required in substantial quantities. The process can reproduce the outside diameter and central hole quickly while using material efficiently. Machining may remain preferable for thick parts, deep three-dimensional forms, unusual internal geometries, or extremely small quantities. The right choice depends on the product’s volume, tolerance, material, geometry, and performance requirements.
Compared with Laser-Cut Parts
Laser cutting provides excellent flexibility during prototype development because it does not require a dedicated stamping die. It can be useful for design verification or small batches. For repetitive mass production, however, the cycle time and operating cost per piece may become less favorable than a purpose-built stamping process.
Once a design is approved and demand is stable, stamping can provide a more efficient production route. A progressive or compound die may complete the central hole and external profile in a rapid sequence. Tooling also provides a physical guide for repeatability, which can support stable dimensions across long production runs.
Compared with Manual Fabrication
Manual cutting, drilling, and forming can be suitable for emergency repair work or very small quantities, but it introduces operator-dependent variation. Hole position, circularity, burr condition, and surface damage may differ from piece to piece. Manual methods also make it difficult to maintain a consistent output when demand increases.
Industrial stamping replaces many individual decisions with controlled tooling and process parameters. This helps customers achieve predictable incoming quality and reduces the time required for inspection, rework, and assembly adjustment.
Engineering Considerations for Customer-Specific Designs
Central Hole Diameter and Fit
The hole diameter should be defined according to the mating component and assembly method. A clearance hole for a bolt requires different considerations from a press-fit hole for a shaft or a hole intended for a rivet. The customer should specify whether the hole must allow free movement, provide a controlled interference fit, or simply support alignment.
Hole tolerance should be coordinated with the material, thickness, production method, and final application. Very tight tolerances may require secondary calibration or additional inspection. If the hole will receive a coating or plating, the thickness of that finish should also be considered when establishing the final fit.
Concentricity and Alignment
For many circular components, the relationship between the center hole and outside diameter is more important than either dimension alone. Poor concentricity can create eccentric rotation, uneven load distribution, or difficulty during automated insertion. Tooling should be designed to maintain the positional relationship between the piercing and blanking operations.
Customers should identify the surfaces that are functionally critical. If the outside edge is only used for clearance, its tolerance may be less demanding than the hole position. If both features guide a rotating assembly, a tighter concentricity requirement may be necessary.
Thickness and Strength
Material thickness affects the part’s rigidity, load distribution, weight, and resistance to deformation. A thicker component may provide greater support but require more stamping force and possibly additional forming considerations. A thinner component may reduce cost and weight but could be more vulnerable to bending or distortion.
The appropriate thickness should be selected based on the expected clamping force, vibration, temperature, contact area, and service life. A technical review can help identify whether the part requires a flat profile, a reinforcing bead, a raised ring, or another feature to obtain the desired performance without unnecessary material consumption.
Flatness and Formed Height
Flatness is important when the component must sit against a mating surface or distribute pressure evenly. Stamping conditions, residual stress, material characteristics, and subsequent forming can influence flatness. If the part is designed with a shoulder or raised feature, the formed height and transition radius should be specified clearly.
Where appropriate, a calibration operation may be included to improve repeatability. The need for calibration should be evaluated against the actual assembly requirement so that the process remains efficient and economical.
Edge Condition and Safety
The edge of the central hole and the outside circumference should be reviewed for contact with operators, wires, seals, moving components, and adjacent surfaces. Sharp edges may cause damage or create handling risks. A controlled chamfer, radius, or deburring operation may be required.
Edge requirements should not be treated as an afterthought. They influence die design, processing time, inspection methods, and packaging. Early definition of the edge condition helps avoid costly changes after tooling has been completed.
Packaging and Identification
Small circular components can become mixed, tangled, scratched, or contaminated if packaging is not planned carefully. Packaging should reflect the part’s size, surface finish, production quantity, and customer handling system. Bulk packaging may be appropriate for robust parts, while counted bags, trays, boxes, or separated layers may be better for delicate or finished components.
Part numbers, batch information, quantity labels, and inspection records can support traceability. Clear identification is particularly valuable when several circular parts have similar outside diameters but different central holes or materials.
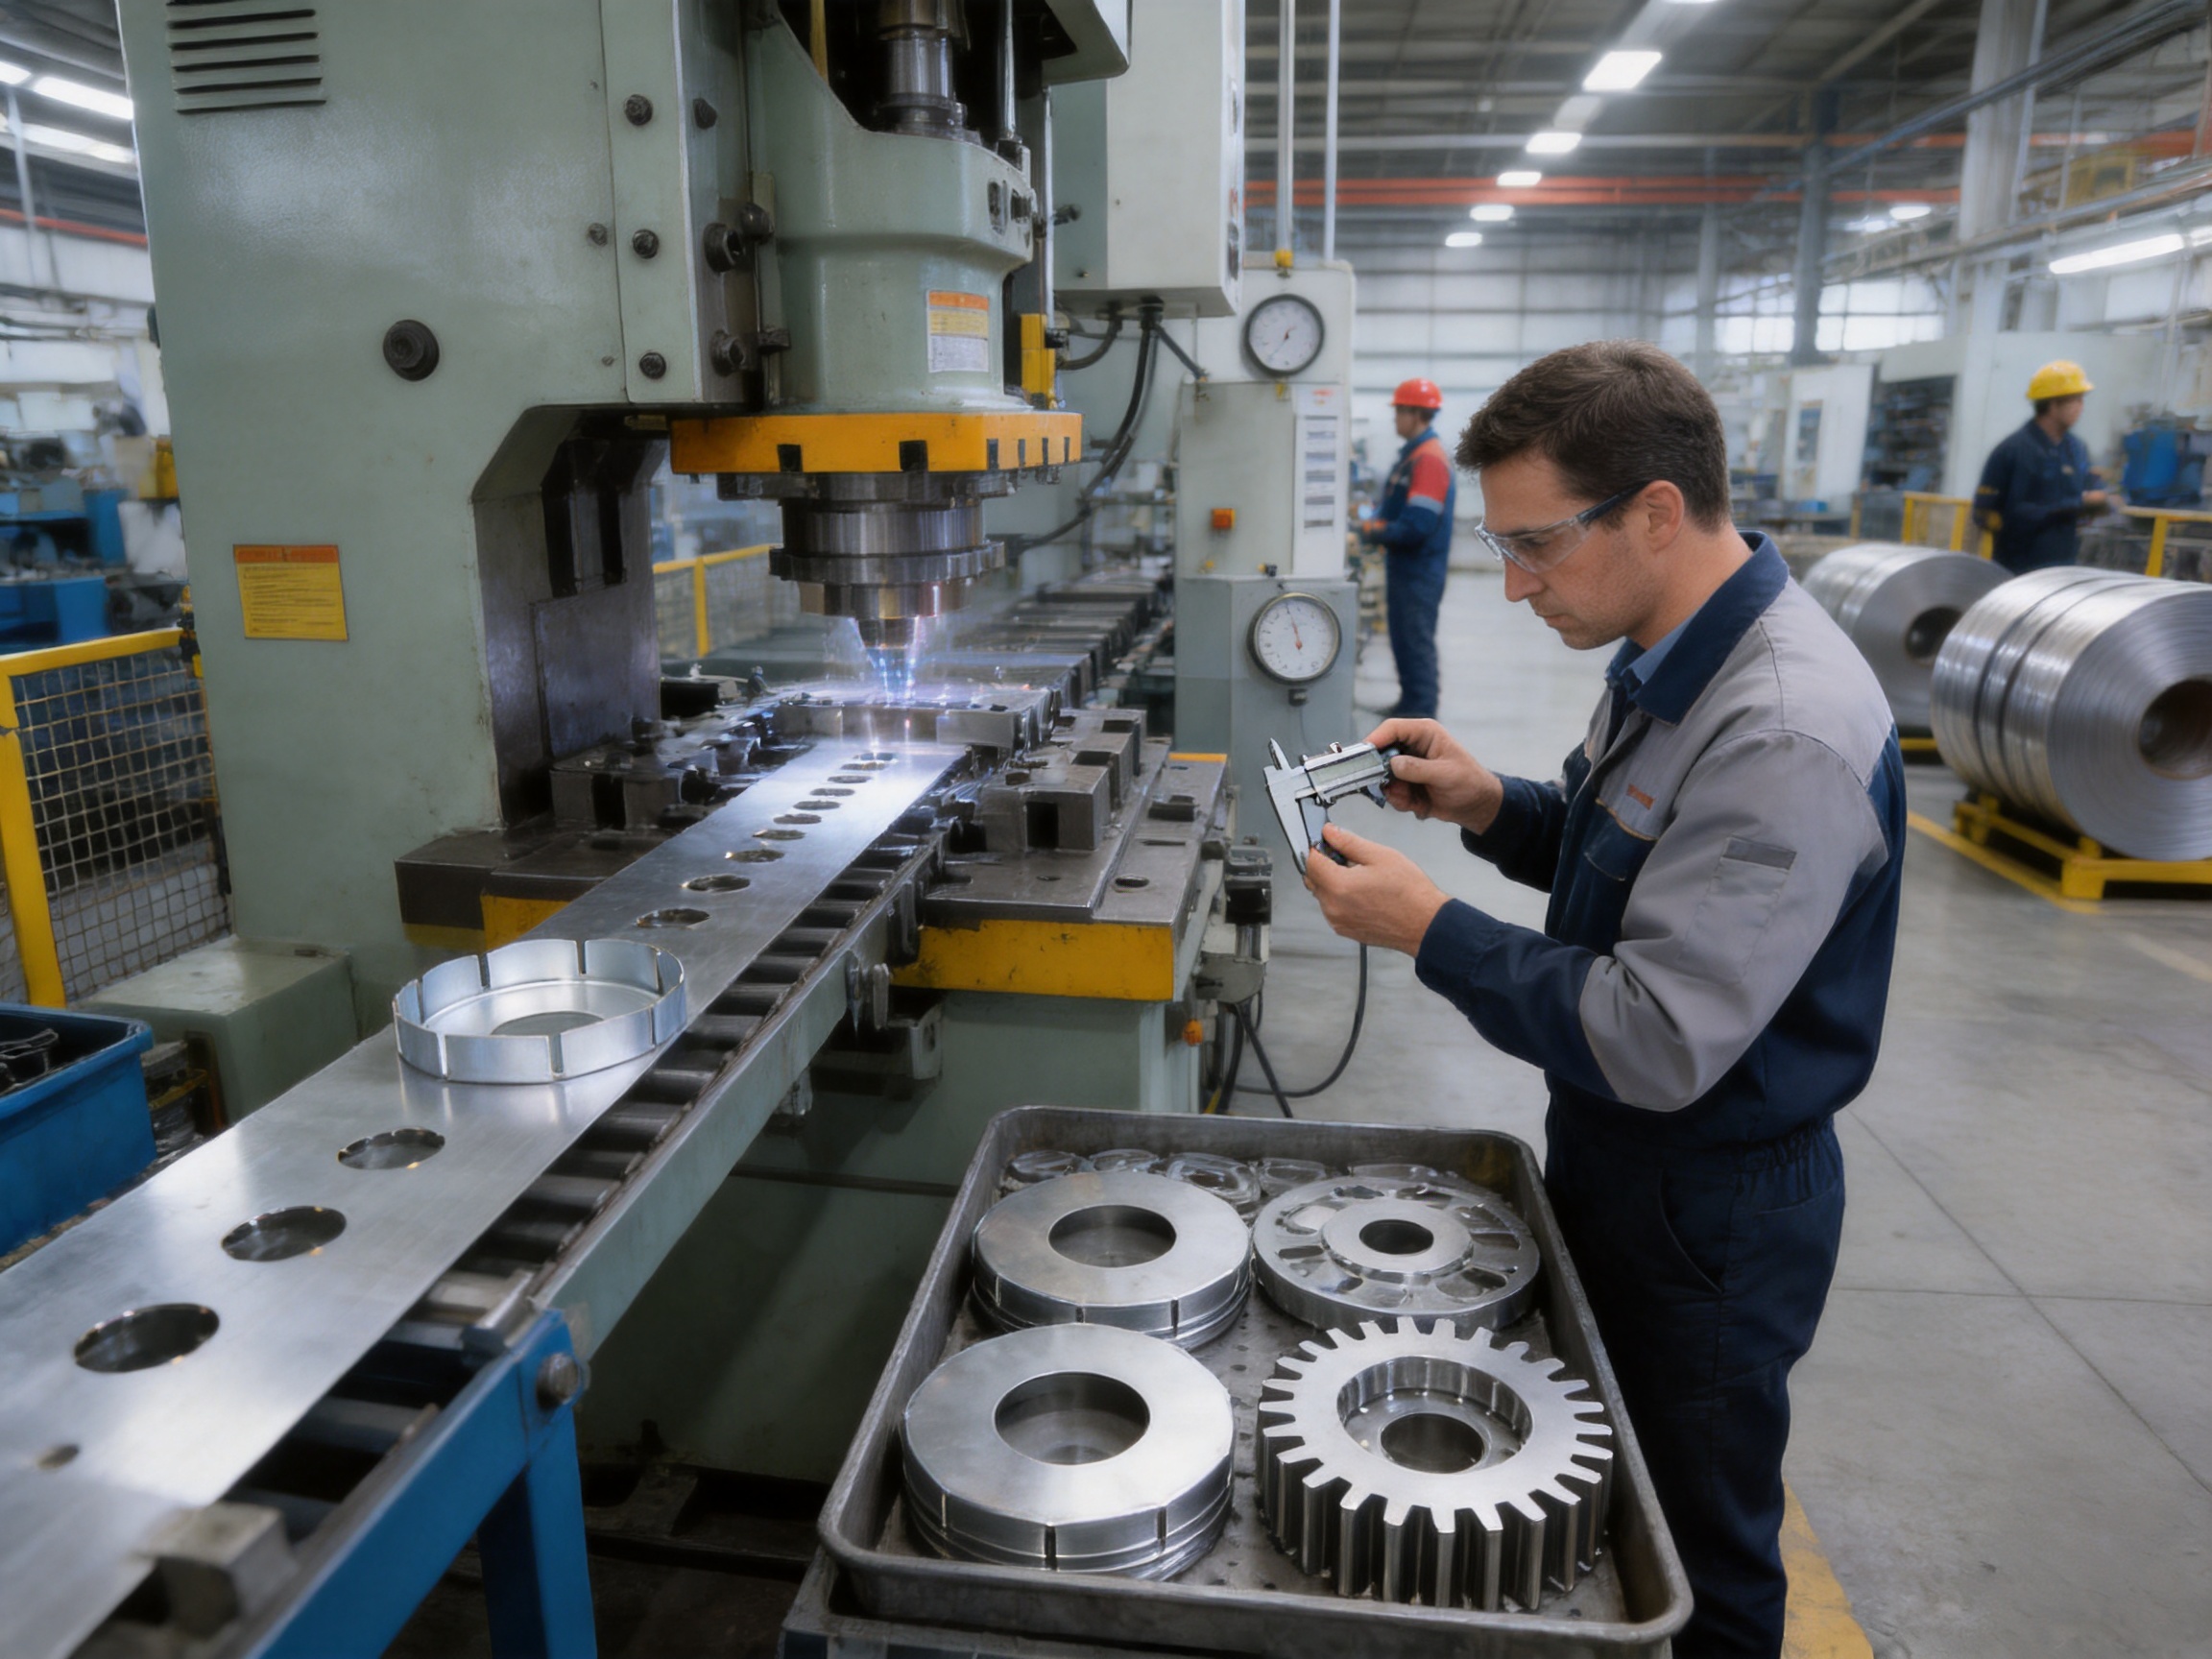
Applications Across Multiple Industries
Automotive Components
Automotive manufacturing uses many small stamped metal parts in brackets, fastening systems, seat structures, interior mechanisms, body hardware, sensor assemblies, and engine-related components. A circular part with a central hole can provide a reliable mounting or spacing function while remaining compact and economical.
Automotive applications often require stable repeatability, resistance to vibration, and dependable fit. Depending on the position of the component, corrosion protection, surface hardness, burr control, and dimensional traceability may also be important. The ability to produce customized parts helps automotive customers integrate the component into a specific vehicle platform or subassembly.
Electrical and Electronic Equipment
Electrical equipment contains numerous mounting, alignment, and fastening points. Circular stamped parts may be used with screws, shafts, terminals, housings, switches, motors, or other internal mechanisms. Material selection may be influenced by conductivity, magnetic response, corrosion resistance, and insulation-related requirements.
The central hole can make the part suitable for mounting a component to a panel or supporting a rotating control. A clean surface and controlled edge condition can help prevent damage to nearby wires, insulation, and delicate components.
Household Appliances
Household electric heaters, small appliances, kitchen appliances, and other domestic products require economical parts that can be assembled efficiently. Circular stamped parts may support knobs, shafts, covers, heating assemblies, hinges, brackets, switches, and internal frames.
Appliance production benefits from a stable supply of consistent components because assembly lines often operate at high speed. Custom stamping allows the manufacturer to match the part to the appliance’s available space, fastening method, heat exposure, and appearance requirements.
Machinery and General Hardware
Machinery manufacturers use stamped components in fixtures, guards, linkages, guides, housings, adjustment mechanisms, and structural connections. In these applications, the central hole may be used with a shaft, pin, bolt, or fastener. The circular outer profile can distribute force or provide a smooth interface between moving parts.
For general hardware products, cost, availability, and consistent dimensions are often key considerations. Stamping provides a scalable production method that can support both customized industrial orders and repeat programs.
Optical and Educational Instruments
Optical instruments and educational equipment may require small metal components for mounting, adjustment, alignment, and structural support. These parts may need careful dimensional control because a small positional error can affect the operation of the finished instrument.
Yuyao Hongli Optoelectronics developed from an enterprise associated with educational instruments and has expanded into broader metal stamping and related manufacturing services. This background supports an understanding of the importance of precise fit, organized assembly, and reliable component supply.
Construction and Building Hardware
Construction-related hardware often requires components that can tolerate handling, fastening pressure, vibration, and variable environmental conditions. Circular stamped parts may be used in brackets, anchors, supports, locks, fixtures, and equipment assemblies. Material and surface treatment can be selected to support the required level of corrosion resistance and service durability.
Manufacturing Strengths and Service Capabilities
Yuyao Hongli Optoelectronics Co., Ltd. is located in Yangming Science and Technology Industrial Park, Yuyao, Zhejiang Province, China. Founded in 2000, the company has accumulated more than two decades of experience in manufacturing and processing metal components and related products.
The company operates a modern factory of approximately 5,000 square meters with multiple stamping workshops and a workforce of more than 60 employees. This production foundation enables the company to manage different product categories and provide services for domestic and international customers. Its capabilities include manufacturing, processing, wholesale, retail, import, and export.
The company’s product range includes educational instruments, optical instruments, household electric heaters, small household appliances, automotive parts, hardware products, plastic products, deep-drawn parts, stamped parts, bending parts, kitchen appliance accessories, and automotive stamping parts. This broad experience is useful when a customer requires more than one type of metal-forming process within the same project.
OEM and ODM Customization
OEM and ODM support allows customers to purchase components made to their own drawings or to collaborate on the development of a new design. For circular stamped parts, customization may include dimensions, material, forming features, surface treatment, inspection requirements, and packaging.
A collaborative process can begin with a review of the customer’s intended use. Engineers can then evaluate whether the proposed geometry is suitable for stamping, identify critical dimensions, and recommend adjustments that may improve manufacturability. This early communication can reduce the risk of tooling changes and production delays later in the project.
Rapid Prototyping and Production Conversion
New products often require prototypes before mass production. A prototype helps verify fit, function, assembly sequence, and appearance. It can also reveal whether the central hole is correctly sized for the mating shaft or fastener and whether the outside diameter provides sufficient clearance.
After the prototype is approved, the design can be transferred into a stable production process. Efficient production conversion requires more than simply making additional pieces. It involves confirming the tooling approach, press capability, material supply, inspection plan, packaging, and delivery schedule. Experience in both development and production helps create a smoother transition from initial sample to repeat order.
Quality and Delivery Management
Consistent quality is supported through technical review, process organization, inspection, and communication. The goal is to ensure that products conform to the approved design and can be delivered according to the customer’s schedule. Stable delivery is particularly important when stamped parts are integrated into a larger assembly line.
Production planning should consider material availability, tooling status, order quantity, inspection requirements, and packaging. Effective coordination helps reduce unexpected interruptions and supports predictable replenishment for long-term customers.
Long-Term Cooperation
The company’s stated business philosophy emphasizes integrity, excellence, innovation, and sharing. For industrial customers, these principles translate into transparent communication, attention to product quality, willingness to improve manufacturing methods, and cooperation throughout the product life cycle.
Long-term cooperation can provide practical benefits. Once a part has been validated, the manufacturing team gains a deeper understanding of its critical features and application. Future orders can then be managed more efficiently, while engineering changes, material substitutions, or volume increases can be evaluated with reference to the established production history.
Quality Management for Reliable Performance
Quality management for circular stamped parts should address the complete supply chain, from raw material through delivery. The material must correspond to the approved grade and thickness. Tooling must be in suitable condition. The press and feeding system must be correctly set. Finished parts must be inspected using methods appropriate to the required tolerance.
Dimensional inspection may include gauges, calipers, micrometers, hole gauges, height gauges, templates, or other equipment selected for the feature being measured. For high-volume production, go/no-go gauges or in-process checking methods may improve speed while maintaining control. More detailed inspection can be applied to first articles, tooling approval samples, or periodic audits.
Visual inspection remains important even when dimensions are correct. Scratches, dents, cracks, excessive burrs, oil residue, discoloration, coating defects, and deformation may affect the finished assembly. Inspection criteria should be defined clearly so that the supplier and customer share the same understanding of acceptable quality.
When the part is used in an important safety-related or high-stress assembly, additional validation may be appropriate. Depending on the application, this may involve load testing, hardness testing, corrosion testing, coating adhesion evaluation, repeated assembly trials, or environmental exposure. The specific validation plan should be developed jointly with the customer.
How to Begin a Custom Circular Stamping Project
Customers can improve project efficiency by providing as much technical information as possible at the beginning. A drawing with tolerances is ideal, but a sample or application description can also serve as a starting point. The following details are especially useful:
1. Required outside diameter and central hole diameter.
2. Material grade, thickness, and mechanical requirements.
3. Required quantity for prototypes, trial production, and regular orders.
4. Flatness, concentricity, burr, and edge requirements.
5. Any formed features, steps, bends, notches, or embossed details.
6. Surface treatment, corrosion resistance, and appearance expectations.
7. Operating temperature, vibration, load, moisture, or chemical exposure.
8. Assembly method and the component that will pass through or contact the central hole.
9. Inspection standards, packaging requirements, and delivery schedule.
With this information, the manufacturer can evaluate the production method, prepare a quotation, recommend material or design adjustments, and establish an appropriate quality plan. If the part is still at the concept stage, an engineering discussion can help determine whether stamping, deep drawing, bending, or a combined process is most suitable.
Q&A About Circular Stamped Parts with a Central Hole
What are circular stamped parts with a central hole used for?
They are used for fastening, spacing, alignment, mounting, load distribution, shaft support, guiding, retaining, and structural connection. Their applications include automotive components, household appliances, electrical equipment, machinery, construction hardware, optical instruments, and general industrial assemblies.
Can the central hole be customized?
Yes. The hole size, position, profile, and related features can be developed according to the customer’s drawing or application requirements. The final design should consider the mating fastener or shaft, material thickness, fit, coating thickness, and required tolerance.
What materials can be used?
Material options depend on the application and the stamping requirements. Common possibilities may include steel, stainless steel, galvanized steel, aluminum, copper alloys, and other suitable sheet metals. The correct material should be confirmed through technical review based on strength, formability, conductivity, corrosion resistance, weight, and cost.
Are these parts suitable for high-volume production?
Yes. Stamping is highly suitable for repeat production when the part geometry is compatible with a die-based process. After tooling is developed and validated, the process can produce consistent parts efficiently and economically, particularly for medium- and large-volume orders.
Can additional features be added to a flat circular part?
Additional features may include raised rings, shoulders, bends, embossments, notches, tabs, countersinks, and other formed details. The available features depend on the material, thickness, part size, tolerance, and tooling design.
How is the quality of the central hole controlled?
Hole quality is controlled through suitable punch and die design, correct clearance, stable material feeding, press alignment, tool maintenance, and inspection. The hole may be checked for diameter, position, burr condition, roundness, and relationship to the outer profile.
Do stamped parts require deburring?
The need for deburring depends on the application and the specified edge condition. Some parts may be acceptable directly after stamping, while others require additional treatment to remove or reduce burrs. The requirement should be defined before production so that the tooling and finishing process can be planned correctly.
Can the parts receive surface treatment?
Yes. Cleaning, polishing, plating, coating, passivation, and other surface treatments may be considered according to the material and operating environment. Surface treatment can improve corrosion resistance, appearance, conductivity, friction behavior, or compatibility with the final assembly.
Can a customer provide a sample instead of a drawing?
A sample can be used as the basis for technical review and quotation. However, a drawing or approved specification is normally recommended before mass production because it defines critical dimensions, tolerances, material, surface condition, and inspection requirements more clearly.
What industries does the manufacturer serve?
The manufacturer serves industries including automotive, electrical, machinery, construction, household appliances, kitchen appliances, optical instruments, educational instruments, and general hardware. Its wider capabilities also include deep-drawn parts, bending parts, plastic products, and related custom components.
How can customers request a quotation?
Customers can provide the part drawing, sample information, material requirements, estimated quantity, surface treatment, packaging expectations, and delivery location. Technical questions can be directed to Yuyao Hongli Optoelectronics Co., Ltd. through hongli@hl-stamping.com or by telephone at +86-13905842349 and +86-13738485724.
Conclusion
Circular stamped parts with a central hole offer a practical combination of precision, strength, compact design, customization, and production efficiency. Their central opening supports a wide range of fastening and alignment functions, while the circular profile allows the component to distribute loads and fit naturally into concentric assemblies. With suitable tooling, material selection, and process control, these parts can provide stable performance over long production runs.
The main advantage of custom stamping is that the part can be designed around the customer’s actual assembly rather than limited to standard component sizes. Hole diameter, outside diameter, thickness, forming details, surface finish, edge condition, and packaging can all be considered as part of an integrated manufacturing solution. Compared with manual fabrication, stamping offers stronger repeatability. Compared with machining or laser cutting, it can provide greater efficiency for suitable medium- and high-volume applications.
Yuyao Hongli Optoelectronics Co., Ltd. supports this product category with more than 20 years of industry experience, a modern 5,000-square-meter factory, multiple stamping workshops, more than 60 employees, OEM/ODM services, rapid prototyping, production conversion, quality control, and international supply capabilities. Its experience in stamped parts, deep-drawn parts, bending parts, kitchen appliance accessories, and automotive stamping parts enables customers to access a broader range of metal-forming solutions from one manufacturing partner.
For companies seeking reliable custom metal components, the most effective approach is to define the functional purpose of the central hole, identify the critical dimensions, select an appropriate material, and review the stamping process early in product development. With clear technical communication and controlled manufacturing, a simple circular component can become a dependable and cost-effective part of a larger industrial system.
References
1. Society of Manufacturing Engineers, Fundamentals of Sheet Metal Stamping and Pressworking.
2. American Society for Metals, Metals Handbook: Forming and Forging.
3. American Society of Mechanical Engineers, Engineering Drawing and Dimensioning Principles.
4. International Organization for Standardization, Quality Management Systems — Requirements.
5. International Organization for Standardization, Geometrical Product Specifications and Dimensional Tolerancing.
6. American Society for Testing and Materials, Standard Practices for Sheet Metal Materials and Mechanical Testing.
7. Technical product information supplied by Yuyao Hongli Optoelectronics Co., Ltd.
Product: Circular stamped parts with a central hole
Previous Post
How High-Quality Air Fryer Parts Improve Cooking Performance and Product Life
Next Post
Precision Stamped Part Extension Cover for Reliable Industrial Protection
News
-
-
What Are Stamped Parts? Stamped parts are metal components produced by pressing flat sheet metal between a die and a punch to cut, bend, or...
READ MORE -
Sheet metal is one of those materials that quietly holds everyday life together. The tray inside your air fryer, the bracket behind a car b...
READ MORE -
Sheet metal bending is one of the most fundamental processes in metal fabrication. It turns a flat sheet of steel, aluminum, or copper into...
READ MORE
Get Fresh Updates Via Email
We promise we will never disclose your email address, and you can opt out at any time.
-
Quick Links
Home About Us Products Service News Contact Us -
Product list
Deep-drawn parts Stamped parts Bending parts Kitchen appliance accessories Automotive stamping parts -
About Us
Factory Honour FAQ -
News
Company News Industry News -
Contact Us
Address: South side of Shunke Road, Yangming Science and Technology Industrial Park, Yuyao City, Zhejiang Province, China Tel: +86-13905842349/+86-13738485724 Email: hongli@hl-stamping.com
Copyright © Yuyao Hongli Optoelectronics Co., Ltd. All Rights Reserved.
Custom Precision-Sheet/Sheet Metal Stamping Manufacturers
