


 English
 русский
 Español
 عربى

What Are Stamped Parts? Stamped parts are metal components produced by pressing flat sheet metal between a die and a punch to cut, bend, or...
READ MORE
News
Home / Author / Chen Ruoxi — Overseas Product Sales Manager / Precision Stamped Circular Parts with Holes for Demanding Industrial Applications
Precision Stamped Circular Parts with Holes for Demanding Industrial Applications
2026-10-20
Stamped circular parts with holes are compact, efficient, and highly adaptable components used in mechanical assemblies, household appliances, automotive systems, optical instruments, educational equipment, and many other industrial products. Although their geometry may appear simple, producing a circular metal component with accurately positioned holes requires careful engineering, suitable material selection, reliable tooling, controlled forming pressure, and consistent inspection. When these factors are managed correctly, the result is a lightweight yet durable part that can support mounting, ventilation, alignment, fastening, spacing, shielding, or structural functions.
Yuyao Hongli Optoelectronics Co., Ltd. manufactures customized stamped circular parts with holes as part of its broad metalworking and precision stamping capabilities. With more than 20 years of industry experience, the company provides solutions for customers that require repeatable dimensions, stable quality, efficient production, and flexible customization. Its product range also includes deep-drawn metal parts, bending parts, kitchen appliance accessories, automotive stamping parts, hardware products, and related components.
For buyers comparing suppliers, the value of a stamped circular part is not determined only by its external appearance. A dependable supplier must understand the part’s intended function, the relationship between diameter and thickness, the required hole pattern, the effects of forming on material strength, and the production volume. The supplier must also be able to turn drawings, samples, or functional descriptions into practical production tooling and repeatable manufacturing procedures.
This article explains the design characteristics, production advantages, applications, quality considerations, and customization potential of stamped circular parts with holes. It also examines how an experienced manufacturing partner can help customers reduce production risk and achieve a more competitive total cost.
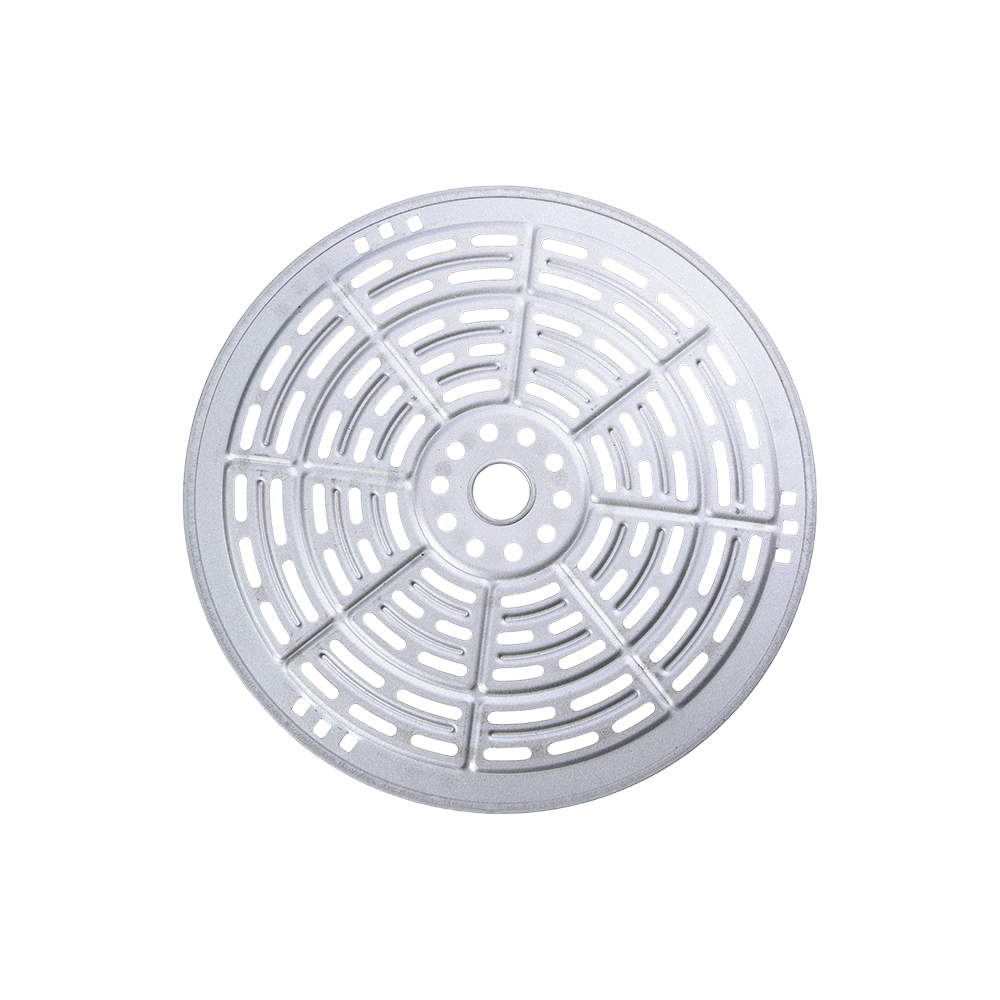
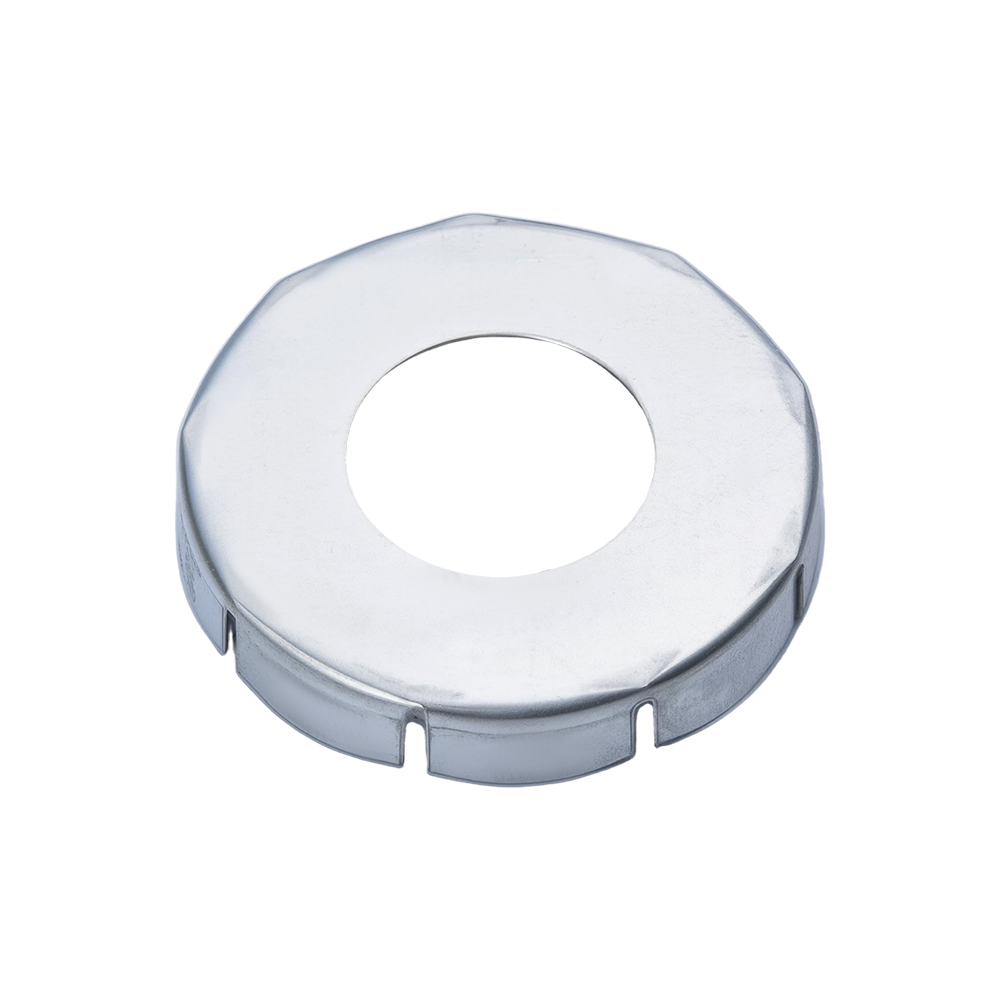
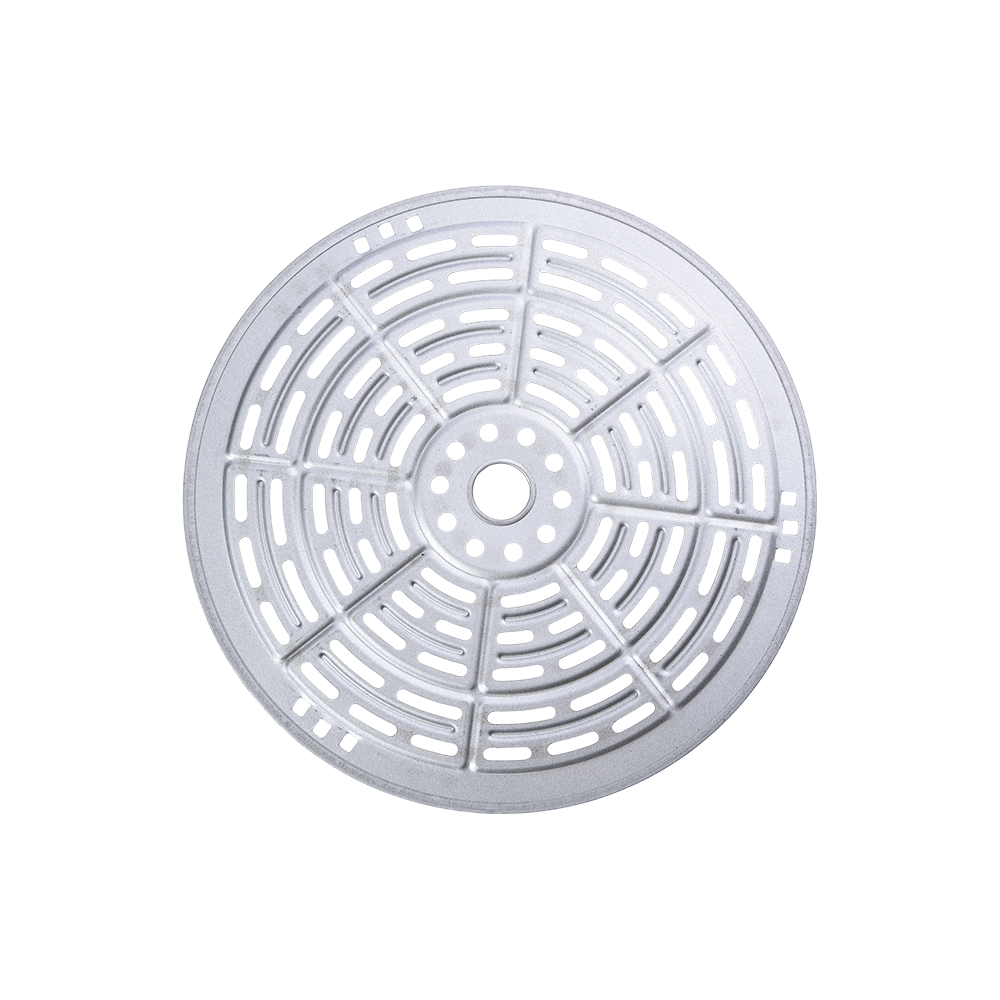
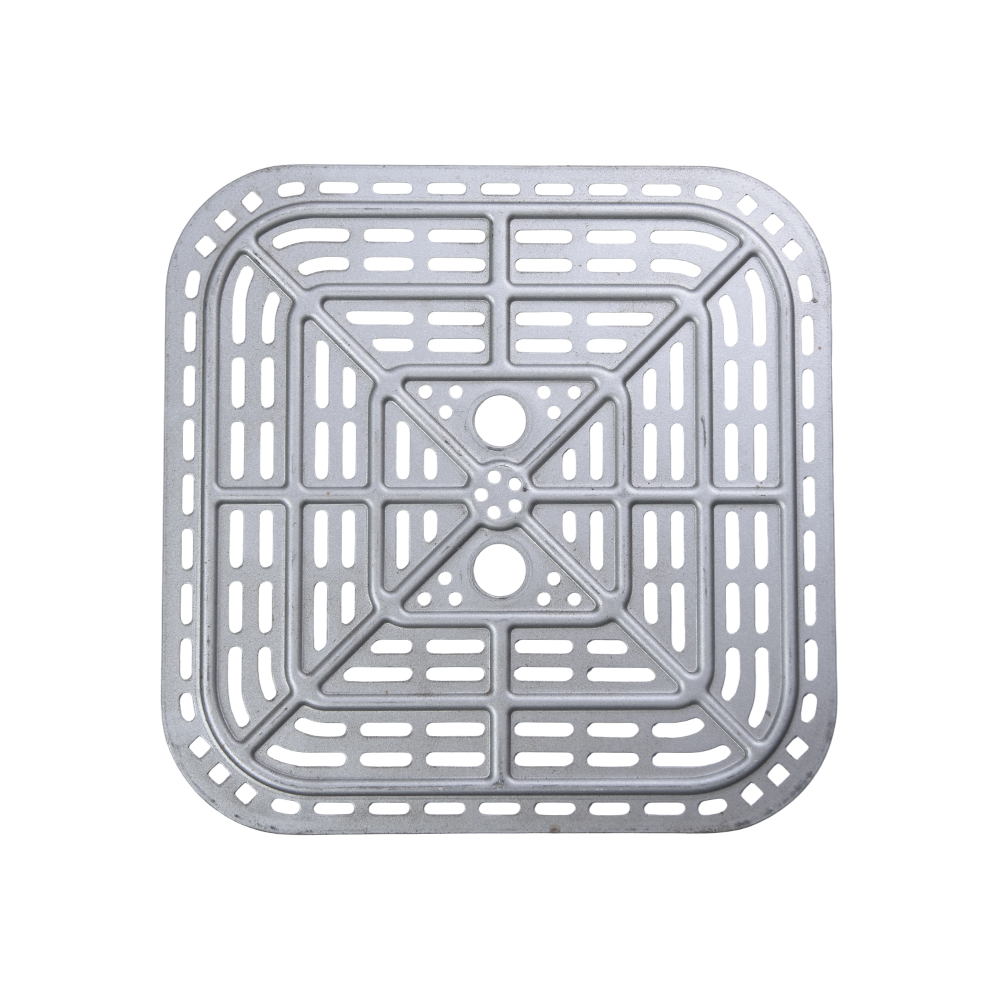
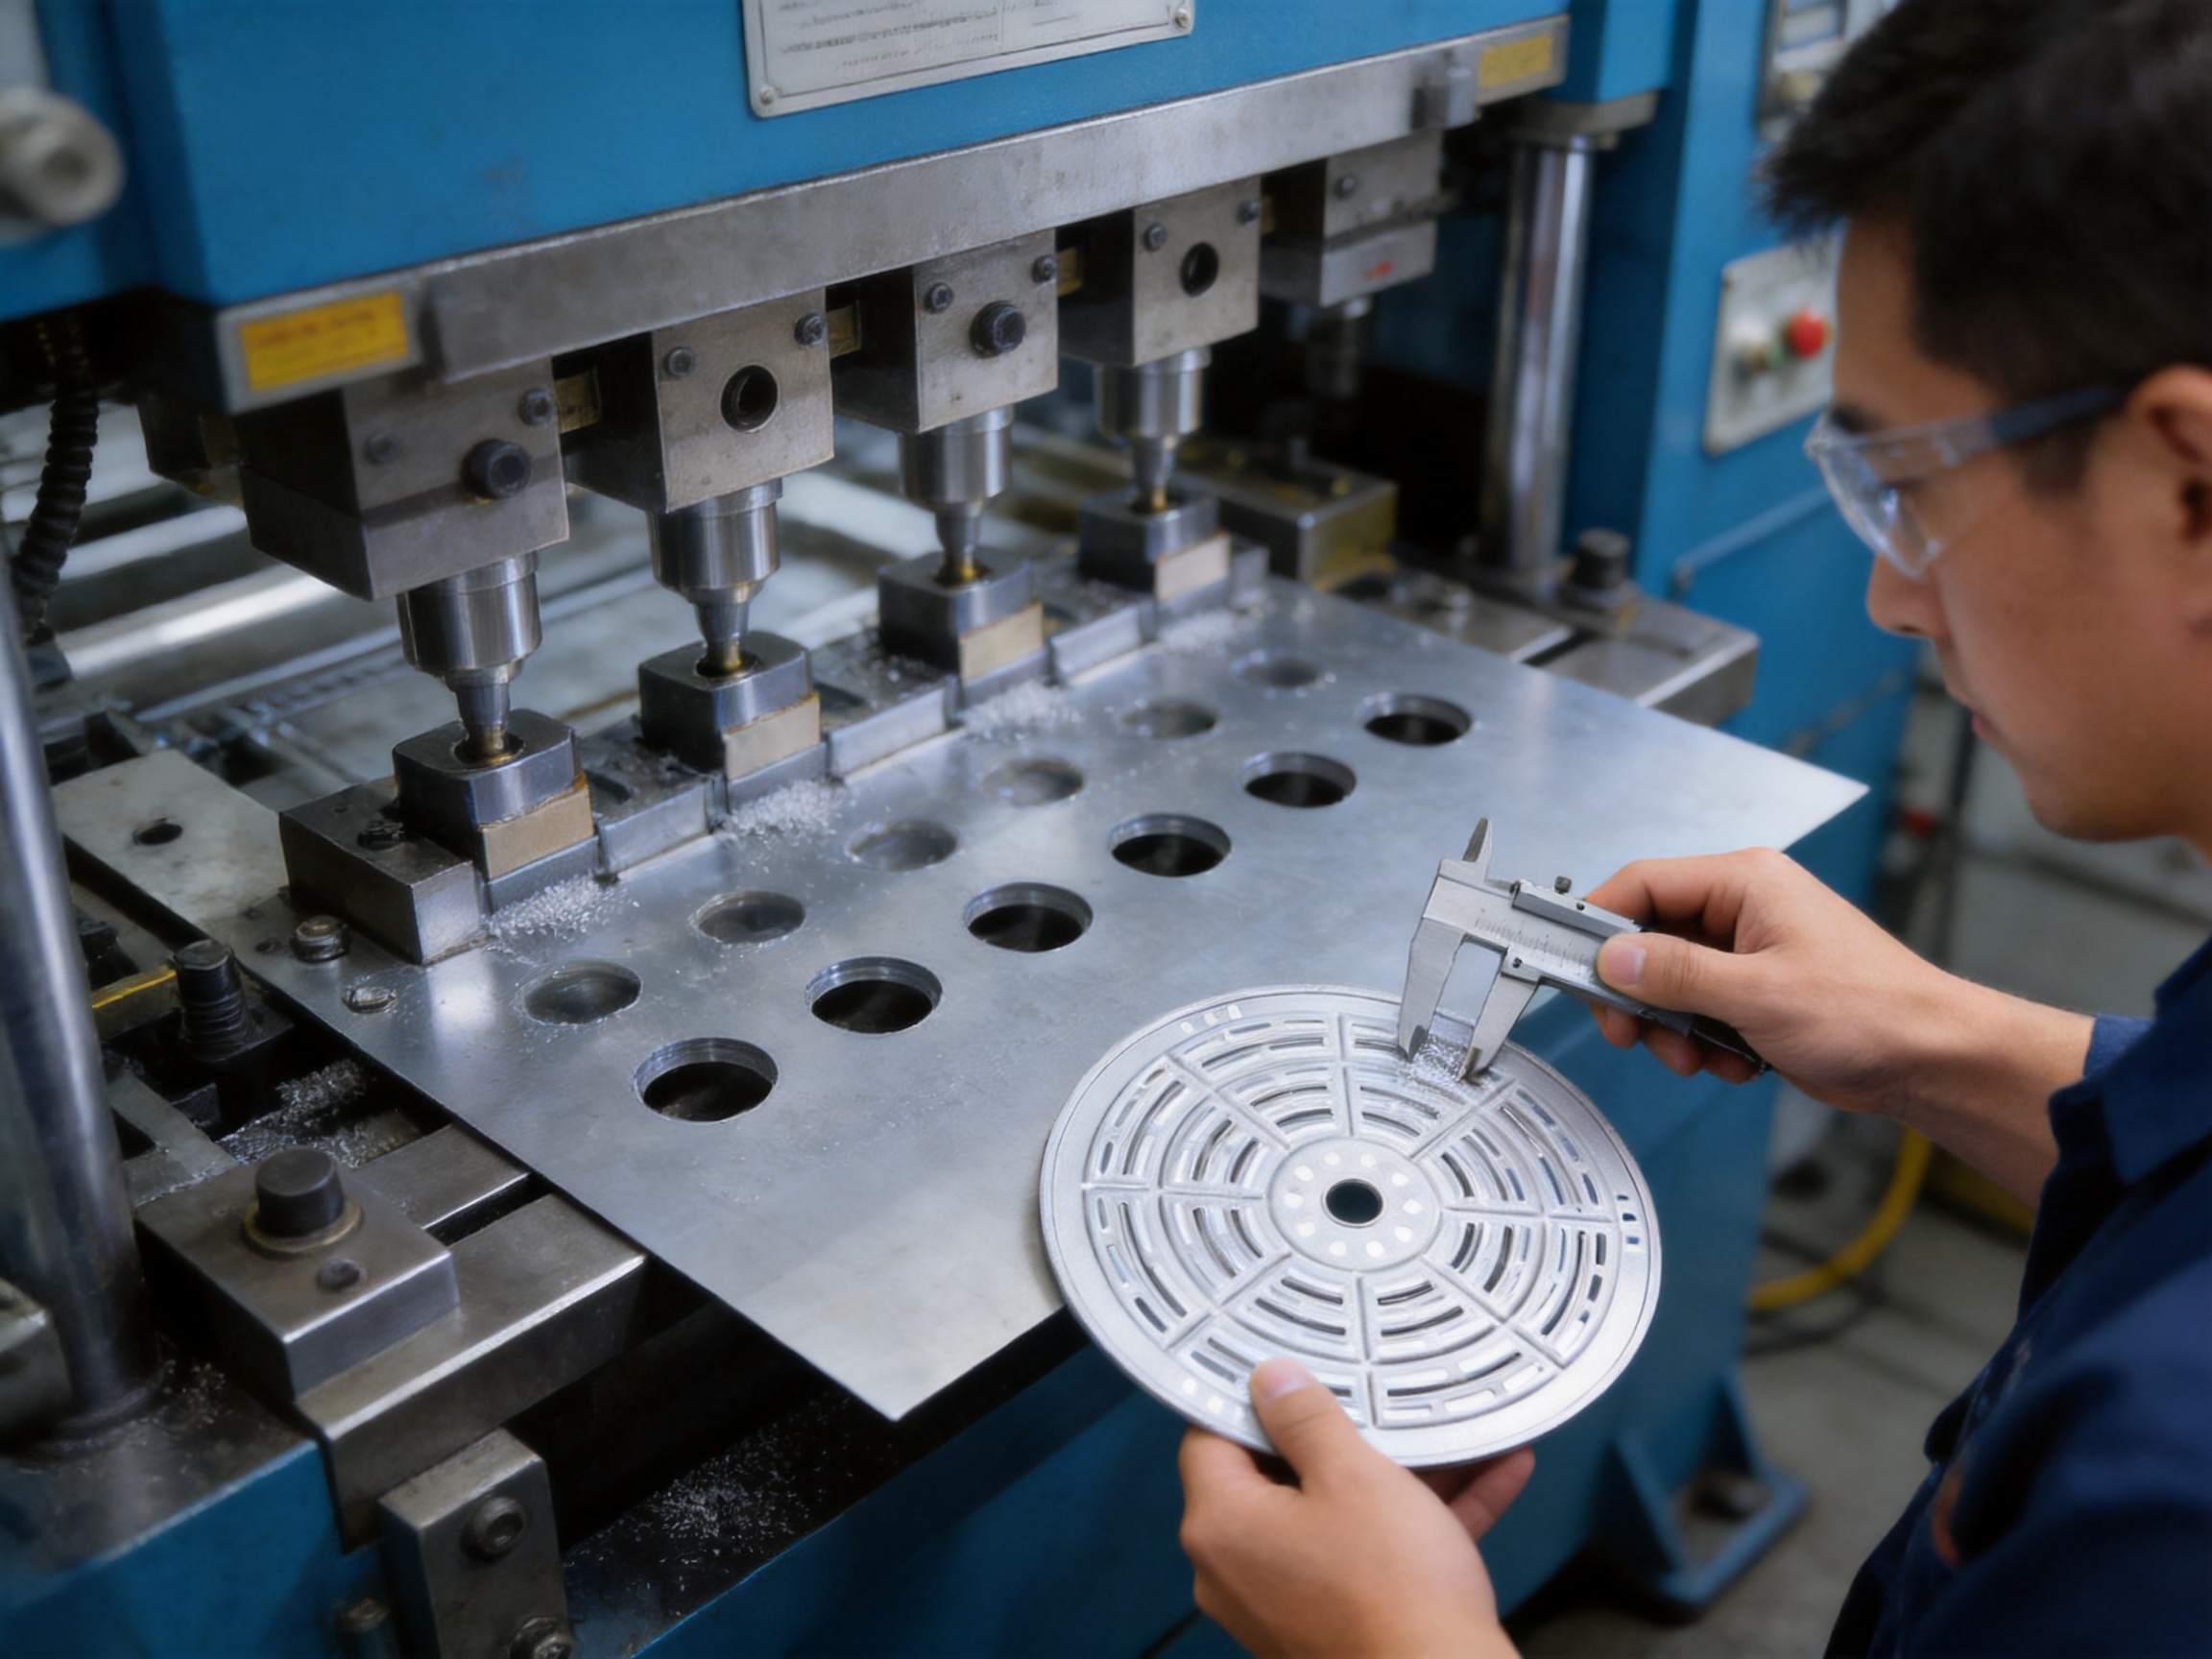
Stamped circular parts with holes
What Are Stamped Circular Parts with Holes?
Stamped circular parts with holes are metal components formed from sheet material through one or more stamping operations. Their basic shape is circular or substantially round, while one or more openings are created within the component. Depending on the design, the part may be flat, slightly formed, recessed, flanged, embossed, or combined with other geometric features.
The holes may be placed at the center, around a circular pitch, along a radial pattern, or in a customized arrangement. They may serve as screw holes, rivet holes, locating holes, ventilation openings, drainage points, cable passages, weight-reduction openings, or assembly features. Hole diameter, spacing, edge distance, and positional tolerance are selected according to the part’s function and the requirements of the finished assembly.
Unlike a manually machined disc, a stamped circular part is produced by applying controlled force through a die and punch. This process allows the manufacturer to form large quantities of similar parts efficiently. Once the tooling has been designed and validated, the production cycle can be highly repeatable, making stamping especially suitable for medium-volume and high-volume orders.
Stamped circular parts can also be integrated with secondary features. These may include raised beads, bent edges, lanced tabs, countersunk areas, embossments, grooves, or shallow drawn sections. The ability to combine several features into a progressive or compound stamping process often reduces the number of separate operations needed during assembly.
Why Circular Stamping Is Valuable
Circular components are common in engineering because they distribute loads efficiently and can fit naturally into rotating, concentric, cylindrical, or housing-based assemblies. Adding carefully positioned holes can reduce weight, permit fastening, improve airflow, or allow other components to pass through the part.
Compared with a solid disc, a perforated stamped component can use less material while retaining the necessary functional area. This can reduce part weight and material consumption. In applications where hundreds or thousands of components are assembled into a product, even a small reduction in weight or material usage can produce meaningful savings.
Stamping also offers a consistent production method. Each part is made using the same tool geometry and operating sequence, which helps maintain uniformity from batch to batch. This repeatability is important when the component must align with a cover, bracket, fastener, shaft, filter, heating element, sensor, or other mating part.
For manufacturers of finished goods, a well-designed stamped circular part can simplify assembly. Accurate holes support automated fastening and locating. Consistent outside diameters improve fit within housings. Clean edges reduce the risk of interference, while formed flanges or beads can increase stiffness without requiring a thicker and heavier material.
Key Advantages Over Alternative Manufacturing Methods
Efficient Production Compared with Machining
Machining a circular part from bar stock or plate can provide excellent dimensional control, but it may remove a considerable amount of material and require longer cycle times. For larger production quantities, machining can therefore result in higher material waste and a higher unit cost.
Stamping forms the component from sheet metal with comparatively little waste. The blanking layout can be planned to use the available sheet efficiently, and multiple parts may be produced from one strip or sheet. This makes stamping an attractive solution when the design can be produced through cutting and forming rather than extensive material removal.
Better Repeatability Compared with Manual Fabrication
Manual cutting, drilling, and bending can be appropriate for prototypes or very small quantities, but it is more dependent on operator skill and may produce variation in hole location, edge quality, flatness, and outside diameter. Stamping uses dedicated tooling to guide the material and define the geometry, providing a more stable process for repeated production.
Lower Weight Compared with Solid Components
Strategically placed holes reduce unnecessary material while preserving the areas required for fastening or load transfer. If the part is designed correctly, the resulting component can be lighter than a solid disc while still meeting the application’s functional needs. This is especially valuable in automotive, portable equipment, and small appliance applications.
Integrated Features Compared with Separate Assembly
A stamped part may combine a circular outline, internal holes, mounting tabs, locating features, and reinforcing beads within one manufacturing sequence. This can reduce the need for separate washers, brackets, spacers, or machined inserts. Fewer individual components may simplify procurement and reduce assembly labor.
Flexible Customization Compared with Standard Parts
Standard washers, discs, and perforated plates may not match the dimensions or hole pattern required by a specialized product. Custom stamping allows the customer to specify the outer diameter, material, thickness, hole size, hole count, hole position, surface treatment, and additional forming features. The result is a part designed for the actual application rather than a compromise based on an existing standard.
Design Features That Can Be Customized
The size, location, and number of holes in stamped circular parts can be adapted to the customer’s drawings or functional requirements. A single central hole may be used for shaft mounting, while several equally spaced holes can support a bolt circle. Asymmetrical hole patterns may be needed to prevent incorrect assembly or to align with an irregular housing.
The outside diameter is another important design parameter. It may be selected to fit inside a cylindrical enclosure, beneath a cover, around a rotating shaft, or against a mating flange. The relationship between the outside diameter and the nearest hole should be reviewed carefully because insufficient edge distance can weaken the part or cause distortion during piercing.
Material thickness affects strength, stiffness, formability, hole quality, and weight. Thin sheet may be appropriate for shielding, ventilation, or lightweight covers, while thicker material may be required for load-bearing brackets or fastening components. The correct thickness depends on the application rather than on appearance alone.
Additional forming features can improve performance. A shallow recess may provide clearance for another component. A raised ring can improve rigidity. A bent outer flange can increase stiffness and support positioning. Embossed areas may create stand-off distance, while small tabs may help retain the part during assembly.
Surface requirements can also be tailored. Depending on the material and service environment, the component may be supplied with a natural metal finish or an additional treatment intended to improve corrosion resistance, appearance, wear performance, or compatibility with other components. Surface treatment should be selected together with the base material and operating conditions.
Materials for Stamped Circular Parts
Material selection should consider strength, ductility, corrosion exposure, temperature, electrical behavior, surface appearance, and forming requirements. Common sheet-metal choices include carbon steel, stainless steel, aluminum, copper, and selected alloy materials. Each material behaves differently under blanking, piercing, bending, and drawing operations.
Carbon steel is frequently selected for general-purpose structural or hardware applications because it offers a useful balance of strength, availability, and cost. It may require a protective surface treatment when exposed to moisture or corrosive environments.
Stainless steel is suitable when resistance to rust and corrosion is especially important. It can also perform well in many kitchen appliance, heating, optical, and industrial applications. However, stainless steel may require careful tool design because its work-hardening behavior can influence forming and tool wear.
Aluminum provides low density and good corrosion resistance, making it useful when weight reduction is a priority. Its lower hardness and different springback behavior must be considered during piercing and forming. Copper and copper alloys may be selected when electrical conductivity, thermal conductivity, or specific contact characteristics are required.
The final material choice should be based on the complete use environment. A part used near a heating element may need to tolerate elevated temperature. A part installed in a humid appliance may require stronger corrosion resistance. An automotive component may encounter vibration, road contaminants, temperature cycling, and repeated assembly forces. A qualified manufacturer can review these conditions before recommending a practical production material.
Manufacturing Process for Circular Stamped Components
1. Requirement Review and Engineering Evaluation
Production begins with a review of the customer’s drawings, samples, specifications, or application description. The manufacturer evaluates the outer profile, hole pattern, thickness, tolerances, forming requirements, material, expected quantity, and surface condition.
This stage is important because a design that appears simple may contain manufacturing risks. Hole locations too close to an edge can cause deformation. Narrow webs between holes may tear during piercing. Tight tolerances on a thin circular part may require additional operations or more precise tooling. A supplier that identifies these issues early can help prevent costly revisions after tooling has been started.
2. Material Preparation
Sheet or coil material is prepared according to the selected production method. Material thickness, width, flatness, surface condition, and mechanical properties are checked as appropriate. Consistent incoming material supports consistent stamping behavior and helps reduce variation during production.
3. Tool and Die Development
The die determines the shape and repeatability of the component. Depending on order volume and design complexity, the part may be produced using a simple die, compound die, progressive die, or a combination of stamping and secondary forming tools.
Tool development considers clearance between punch and die, cutting direction, material flow, support surfaces, stripping, part removal, and expected tool life. Proper clearance is essential for achieving clean hole edges and minimizing burrs. The tool must also provide adequate support so that the circular blank does not distort during piercing or forming.
4. Blanking and Piercing
Blanking creates the external circular profile, while piercing creates the internal holes. These operations may occur separately or within the same die, depending on the component and production plan. The sequence is selected to reduce distortion and maintain the required relationship between the outer diameter and hole pattern.
Hole quality is influenced by material type, thickness, punch sharpness, die clearance, press alignment, and production speed. A properly managed process produces a defined sheared zone and controlled fracture zone, with burrs kept within the agreed specification.
5. Forming and Secondary Operations
If the component includes a recess, flange, bead, or angled section, forming operations follow blanking and piercing or are integrated into the same tool. Forming pressure must be controlled to avoid cracking, wrinkling, excessive thinning, or unwanted distortion.
Some components may require deburring, flattening, cleaning, surface treatment, inspection, or packaging after stamping. The production route is selected according to the part’s function and the customer’s quality requirements.
6. Inspection and Process Verification
Inspection may include measurement of outside diameter, hole diameter, hole position, flatness, height, material thickness, edge condition, and surface appearance. Visual checks can identify scratches, cracks, deformation, oil contamination, or other abnormalities.
For repeat orders, process records and inspection feedback help maintain consistency. When a customer has special critical dimensions, those dimensions can be identified for closer monitoring during production.
Manufacturing Strengths of an Experienced Supplier
Yuyao Hongli Optoelectronics Co., Ltd. has more than 20 years of experience in manufacturing metal stamping parts and related products. Founded in 2000, the company has developed from its former educational-instrument business into a comprehensive manufacturer serving multiple industrial sectors.
The company operates a modern factory of approximately 5,000 square meters and has more than 60 employees. Its production capabilities cover stamping workshops and related processing activities for educational instruments, optical instruments, household electric heaters, small household appliances, auto parts, hardware products, plastic products, deep-drawn parts, bending parts, kitchen appliance accessories, and automotive stamping parts.
This broad product experience is valuable because different industries place different demands on metal components. Optical equipment may require accurate alignment and clean appearance. Household appliances may require corrosion resistance and stable fit. Automotive parts may require robust forming, repeatability, and resistance to vibration. Experience across these categories helps the manufacturing team understand how a stamped component functions within a larger product.
The company supports OEM and ODM customization, allowing customers to provide drawings, samples, specifications, or product concepts. It also supports rapid prototyping and efficient production conversion. These capabilities are useful when a customer needs to confirm fit and function before committing to a larger production run.
Quality Advantages and Production Reliability
Quality in stamped circular parts is a combination of dimensional accuracy, material consistency, edge condition, surface quality, structural integrity, and repeatability. A part may look acceptable while still having a hole-position error, excessive burr, hidden crack, or distortion that creates problems during assembly. For this reason, reliable production requires more than a final visual inspection.
A controlled stamping process begins with suitable material and properly maintained tooling. Press alignment and operating conditions must remain stable. Operators must understand the process and identify abnormal conditions promptly. Finished parts should be handled and packaged in a way that prevents deformation, scratching, or contamination.
Hongli emphasizes strict quality control, stable delivery, and comprehensive after-sales service. These strengths are important for customers that depend on predictable production schedules. A supplier’s ability to communicate clearly, manage production changes, and respond to quality questions can be as important as the original tooling and stamping capability.
For international customers, dependable export coordination is also valuable. Clear documentation, consistent packaging, production updates, and responsive communication help reduce uncertainty throughout the purchasing process. A supplier that offers manufacturing, processing, wholesale, retail, import, and export services can support different purchasing models and customer requirements.
Performance in Demanding Environments
Stamped circular parts with holes may be installed in environments involving moisture, heat, dust, vibration, cleaning agents, or contact with dissimilar materials. The design and material must therefore be selected according to actual service conditions.
Rust resistance is particularly important for appliance accessories, hardware, and components exposed to humidity. Stainless steel or a suitable protective finish may be selected depending on the intended environment. Corrosion resistance helps preserve the hole dimensions, edge integrity, and appearance over time.
High-temperature resistance can be important for parts used near household electric heaters, heating elements, engine compartments, or thermal equipment. The selected metal must retain suitable strength and dimensional stability at the expected operating temperature. Coatings, lubricants, and adjoining materials should also be reviewed because they may respond differently to heat.
In vibrating applications, hole edges and narrow webs should be designed to avoid stress concentration. A suitable edge distance, rounded transition, and adequate material thickness can improve fatigue performance. If the part is fastened, the joint design should prevent excessive localized stress around the holes.
For corrosive environments, the customer should provide information about humidity, salt exposure, chemicals, cleaning procedures, and expected service life. This allows the supplier to recommend a more appropriate combination of metal, thickness, forming method, and surface protection.
Applications Across Multiple Industries
Household Appliances
Stamped circular parts with holes are used in small household appliances, electric heaters, ventilation assemblies, protective covers, brackets, and internal support structures. Openings may support airflow, fastening, heat dissipation, or the passage of wires and mechanical components.
Kitchen appliance accessories may require clean edges, corrosion resistance, attractive appearance, and compatibility with repeated cleaning. Circular stamped components can serve as mounting plates, protective screens, support rings, or internal hardware.
Automotive Components
Automotive stamping parts must often withstand vibration, temperature changes, moisture, and demanding assembly conditions. Circular components with holes may be used as mounting plates, brackets, shields, spacers, retainers, or support elements. Hole accuracy is important when the component is attached to a vehicle structure or aligned with other hardware.
Optical Instruments
Optical instruments may use stamped metal components for mounting, spacing, shielding, or internal support. In these applications, dimensional stability and clean surfaces can be important because an improperly positioned component may affect alignment or interfere with sensitive parts.
Educational Instruments
Educational equipment often includes mechanical frames, demonstration devices, optical assemblies, and small electrical systems. Custom stamped parts can provide economical structural and mounting solutions for repeated production.
General Hardware and Industrial Equipment
Industrial machinery, control boxes, ventilation systems, lighting products, and general hardware may use circular stamped components for fastening, spacing, guarding, and reinforcement. Custom hole patterns allow the part to fit a particular equipment layout without additional drilling or modification.
| Application Area | Typical Function | Important Considerations |
|---|---|---|
| Household appliances | Mounting, ventilation, shielding, support | Corrosion resistance, clean edges, stable fit |
| Automotive systems | Brackets, retainers, spacers, shields | Strength, vibration resistance, hole accuracy |
| Optical instruments | Alignment, spacing, internal support | Dimensional control, surface condition, flatness |
| Heating equipment | Heat shielding, mounting, structural support | Temperature resistance, material stability |
| General hardware | Fastening, reinforcement, equipment assembly | Cost efficiency, repeatability, corrosion protection |
How to Specify a Custom Part
A clear specification helps the supplier evaluate feasibility and prepare an accurate quotation. The customer should provide a two-dimensional drawing when available, including the outside diameter, hole diameters, hole positions, material thickness, tolerances, and any formed features.
If a drawing is not available, a sample, sketch, photograph, or functional description may be used as a starting point. The customer should explain where the part will be installed, how it will be fastened, what loads it will experience, and whether it will encounter heat, moisture, chemicals, or vibration.
Important information includes the required annual or monthly quantity, target delivery schedule, packaging preferences, surface requirements, and inspection expectations. It is also useful to distinguish critical dimensions from non-critical dimensions. This helps the manufacturer focus tooling and process control where it has the greatest effect on product performance.
Customers should not specify unnecessarily tight tolerances without a functional reason. Very tight tolerances may require additional operations, slower production, specialized inspection, or more expensive tooling. A practical tolerance strategy can provide reliable assembly while maintaining a competitive total cost.
Cost and Supply Chain Benefits
The unit price of a stamped circular part depends on material, thickness, part size, hole count, tooling complexity, production volume, tolerance requirements, surface treatment, packaging, and inspection. A low initial quotation is not always the lowest total cost if it leads to inconsistent parts, late delivery, repeated sorting, or assembly problems.
A capable stamping manufacturer can help reduce total cost through material utilization, efficient tooling, integrated operations, and stable process control. If blanking, piercing, and forming can be combined effectively, the number of handling steps may be reduced. When the production process is stable, fewer defective parts and less rework can improve the overall economics of the project.
OEM and ODM support can also reduce the burden on the customer’s engineering team. Instead of searching separately for tooling, stamping, finishing, and export coordination, the customer may work with one manufacturing partner for a broader range of requirements.
Stable delivery is especially important for customers operating assembly lines. Delayed stamped components can interrupt production and create additional logistics costs. A supplier with established workshops, experienced employees, and organized production planning is better positioned to support recurring orders and schedule changes.
Prototyping and Production Conversion
Before mass production, a prototype or trial batch can confirm the relationship between the stamped part and the finished assembly. This stage may reveal issues involving hole alignment, interference, flatness, fastening force, surface contact, or installation sequence.
Rapid prototyping helps customers evaluate the design without waiting for a long production cycle. The prototype may be produced using preliminary tooling or a limited production setup, depending on the part geometry and quantity required. Feedback from testing can then be incorporated into the final tool design.
Production conversion requires more than copying a prototype. The manufacturer must ensure that the final tooling can produce the approved geometry repeatedly and economically. Material flow, press capacity, tool durability, production speed, and inspection procedures should all be reviewed before the full order is released.
Hongli’s experience with OEM and ODM projects supports this transition from concept to repeat production. Its manufacturing and processing capabilities allow the company to work with different product categories and adapt the production approach to the customer’s specific requirements.
Environmental and Resource Efficiency Considerations
Stamping can support more efficient use of raw material when the part layout is carefully designed. Nesting circular blanks and managing the arrangement of internal holes can reduce scrap. Although some material remains as skeleton scrap or slug waste, the overall process can be more efficient than machining a complete disc from a larger solid block.
Lightweight designs can also reduce the material required for each component and lower the weight of the finished product. In automotive and portable equipment applications, this may contribute to broader product-efficiency goals.
Tool maintenance and process stability are additional resource considerations. Well-maintained tooling produces more consistent parts and reduces the need for rework or sorting. Proper packaging protects components during transportation and helps prevent damage that would otherwise create unnecessary waste.
Customers seeking a more sustainable solution should discuss material utilization, recycled content where appropriate, surface-treatment requirements, packaging, and expected service life with the supplier. A durable component that performs reliably for a long period can provide greater practical value than a lower-cost component requiring early replacement.
Common Quality Problems and Their Prevention
Excessive Burrs
Burrs may result from incorrect die clearance, worn punches, unsuitable material conditions, or poor alignment. They can interfere with assembly, create a safety concern, or damage adjacent components. Correct tooling and timely maintenance help reduce burr formation.
Hole Deformation
Hole distortion may occur when the material is not adequately supported or when piercing is performed too close to an edge or another opening. Reviewing hole spacing and using suitable tool support can improve the result.
Part Warping
Warping may result from uneven forming pressure, residual stress, thin material, or an unsuitable operation sequence. Flattening or restriking operations may be used when required, but the best solution is often to address the root cause during tool and process development.
Cracks and Splitting
Cracks can be associated with excessive forming, low material ductility, sharp corners, or incorrect process conditions. Rounded transitions, suitable material selection, and controlled forming can lower the risk.
Dimensional Variation
Variation can be caused by material changes, tool wear, press instability, or inconsistent setup. Routine inspection and process monitoring help identify changes before they affect a large quantity of parts.
Surface Damage
Scratches, dents, and discoloration may occur during stamping, handling, storage, or transportation. Protective handling methods, clean tooling, suitable lubrication, and proper packaging can help preserve surface quality.
Why Choose a Specialized Manufacturing Partner?
A specialized stamping manufacturer brings more than production equipment. It brings practical knowledge about how materials behave, how holes should be positioned, how dies should be designed, and how a part can be made efficiently at the required volume.
For stamped circular parts with holes, this expertise directly affects performance. A supplier that understands only the basic outline may overlook the influence of hole spacing, edge distance, forming sequence, burr direction, or fastening loads. An experienced supplier can review the complete application and suggest improvements that make the part easier to manufacture and more reliable in use.
Yuyao Hongli Optoelectronics combines long-term industry experience, a modern factory, multiple stamping workshops, a workforce of more than 60 employees, and broad product-category knowledge. Its capabilities extend from standard stamped parts to customized deep-drawn, bent, and automotive components. This range supports customers that require more than one type of metalworking operation or plan to develop related products over time.
The company’s business philosophy emphasizes integrity, excellence, innovation, and sharing. In practical terms, these principles support an approach based on transparent communication, continuous improvement, customized solutions, and long-term cooperation. The objective is not simply to produce one batch of parts, but to provide dependable manufacturing support throughout product development and ongoing supply.
Ordering and Cooperation Process
The cooperation process generally begins with an inquiry containing the drawing, sample, specification, or application details. The supplier reviews the information and discusses material, dimensions, quantity, tooling, surface requirements, inspection, packaging, and delivery.
After the technical details are clarified, the manufacturer can prepare a quotation and production proposal. If the project requires tooling, the tool design and production schedule are reviewed before manufacturing begins. A trial sample or first article can then be evaluated by the customer.
Once the sample is approved, the supplier organizes repeat production according to the agreed specifications. Quality checks are performed during the process, and finished components are packaged for delivery. For continuing orders, communication regarding forecasts, revisions, and delivery schedules helps maintain supply stability.
Customers should communicate design changes as early as possible. A change in hole diameter, material thickness, surface treatment, or outside profile can affect tooling and production conditions. Early communication allows the supplier to evaluate the change and avoid producing parts to an outdated specification.
Questions and Answers
What are stamped circular parts with holes used for?
They are used for mounting, fastening, ventilation, shielding, alignment, spacing, weight reduction, drainage, and structural support. Applications include household appliances, automotive parts, optical instruments, heating equipment, educational instruments, and general industrial hardware.
Can the hole size and position be customized?
Yes. The number, diameter, spacing, and location of holes can be customized according to the customer’s drawing or application requirements. Central holes, bolt-circle patterns, radial arrangements, and irregular patterns can all be considered during tool development.
What materials can be used?
Common options include carbon steel, stainless steel, aluminum, copper, and other suitable sheet-metal alloys. The best material depends on strength, corrosion exposure, temperature, electrical requirements, appearance, and forming behavior.
Are these components suitable for high-temperature applications?
They can be suitable when the material, thickness, forming method, and surface treatment are selected for the expected operating temperature. Customers should provide detailed temperature and exposure information so the manufacturer can evaluate the application properly.
Can additional features be added to a circular stamped part?
Yes. Depending on the design, features such as flanges, beads, recesses, tabs, embossments, grooves, and formed edges may be added. These features can improve rigidity, positioning, clearance, or assembly performance.
What information is needed for a quotation?
A drawing or sample is preferred, together with material, thickness, dimensions, tolerances, surface requirements, estimated quantity, packaging needs, and delivery expectations. If a drawing is unavailable, a sketch and description of the part’s function can be used for an initial review.
Can the supplier support prototypes?
Yes. Prototype and trial production support can help verify dimensions, fit, function, and assembly before larger-scale manufacturing. The final process is then adjusted as needed for stable and efficient production.
How can burrs and deformation be controlled?
Tool clearance, punch condition, die support, material selection, press alignment, and operation sequence all influence burrs and deformation. Proper tooling development and process inspection are essential for controlling these issues.
Why is hole position important?
Hole position affects fastening, alignment, load distribution, assembly speed, and clearance from nearby features. Even a small positional error may create problems when the part is installed in a precise assembly, so hole locations should be identified as critical dimensions when necessary.
What makes an experienced stamping supplier valuable?
An experienced supplier can identify design risks, select suitable materials, develop practical tooling, manage secondary operations, control quality, support prototypes, and maintain stable production. These capabilities help reduce delays, rework, and total project cost.
Conclusion
Stamped circular parts with holes provide an effective combination of precision, low weight, production efficiency, and design flexibility. Their circular geometry supports many mechanical and structural applications, while customized openings allow the component to perform fastening, ventilation, alignment, drainage, shielding, and weight-reduction functions.
Compared with machined, manually fabricated, or assembled alternatives, stamped components can offer better repeatability, lower material waste, faster production, and easier integration of multiple features. Their performance depends on thoughtful design, appropriate material selection, accurate tooling, controlled forming, and reliable inspection.
Yuyao Hongli Optoelectronics Co., Ltd. offers customized stamped circular parts with holes supported by more than 20 years of industry experience, a 5,000-square-meter factory, multiple stamping workshops, more than 60 employees, OEM and ODM services, rapid prototyping, strict quality control, stable delivery, and broad expertise in metal products. These capabilities make the company a practical partner for customers seeking precision-sheet and sheet-metal stamping solutions.
Whether the requirement involves a simple perforated disc, a formed circular mounting plate, an automotive stamping component, a kitchen appliance accessory, or a specialized industrial part, early technical communication is the foundation of a successful result. By sharing accurate drawings, application conditions, quantity forecasts, and performance expectations, customers can work with the manufacturer to develop parts that are reliable, economical, and suitable for long-term production.
References
1. Society of Manufacturing Engineers, Fundamentals of Sheet Metal Forming and Stamping.
2. American Society of Mechanical Engineers, General Principles of Dimensional and Geometric Control in Manufactured Components.
3. American Iron and Steel Institute, Sheet Steel Product and Forming Considerations.
4. International Organization for Standardization, Quality Management Principles for Manufacturing Operations.
5. Metal Forming Handbook, Principles of Blanking, Piercing, Bending, and Deep Drawing.
6. Manufacturing Engineering Reference Guide, Tool Design and Process Control for Pressworking.
7. Materials and Processes in Manufacturing, Sheet-Metal Materials, Surface Engineering, and Production Planning.
Product: Stamped circular parts with holes
Previous Post
High-Performance Air Fryer Containers for Reliable Everyday Cooking
Next Post
Precision Stamped Miniature Parts for Demanding Industrial Applications
News
-
-
When you need a metal component whose depth clearly exceeds its width, such as a one-piece battery enclosure, an air-fryer inner container,...
READ MORE -
Steel is the backbone of modern manufacturing, yet it is never a single, uniform material. When engineers and buyers ask, "How can you clas...
READ MORE -
Sheet metal is one of those materials that quietly holds everyday life together. The tray inside your air fryer, the bracket behind a car b...
READ MORE
Get Fresh Updates Via Email
We promise we will never disclose your email address, and you can opt out at any time.
-
Quick Links
Home About Us Products Service News Contact Us -
Product list
Deep-drawn parts Stamped parts Bending parts Kitchen appliance accessories Automotive stamping parts -
About Us
Factory Honour FAQ -
News
Company News Industry News -
Contact Us
Address: South side of Shunke Road, Yangming Science and Technology Industrial Park, Yuyao City, Zhejiang Province, China Tel: +86-13905842349/+86-13738485724 Email: hongli@hl-stamping.com
Copyright © Yuyao Hongli Optoelectronics Co., Ltd. All Rights Reserved.
Custom Precision-Sheet/Sheet Metal Stamping Manufacturers
